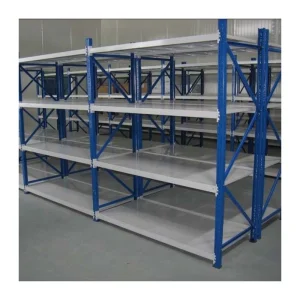
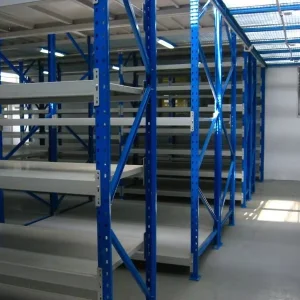
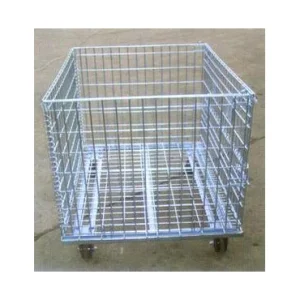
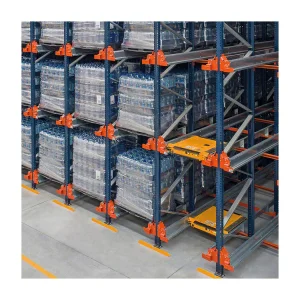
Explore our elite portfolio of heavy-duty pallet racks, mezzanine flooring, and customizable modular storage units built for enterprise-grade performance.
Established in 2015, Ningbo Xinmiao Storage Equipment Co., Ltd. represents the absolute gold standard in heavy-duty pallet racking and intelligent warehouse logistics solutions.
Established in 2015, Ningbo Xinmiao Storage Equipment Co., Ltd. is a leading manufacturer specializing in heavy-duty pallet racking, industrial shelving, and intelligent warehouse storage systems. Spanning a modern manufacturing facility of over 35,000 square meters, we have dedicated over 14 years to the industry, providing robust and reliable storage solutions to global enterprise clients. With 8 years of direct export experience, our products are trusted in key markets across North America, Europe, Southeast Asia, and the Middle East, generating an annual export revenue exceeding $18 million.
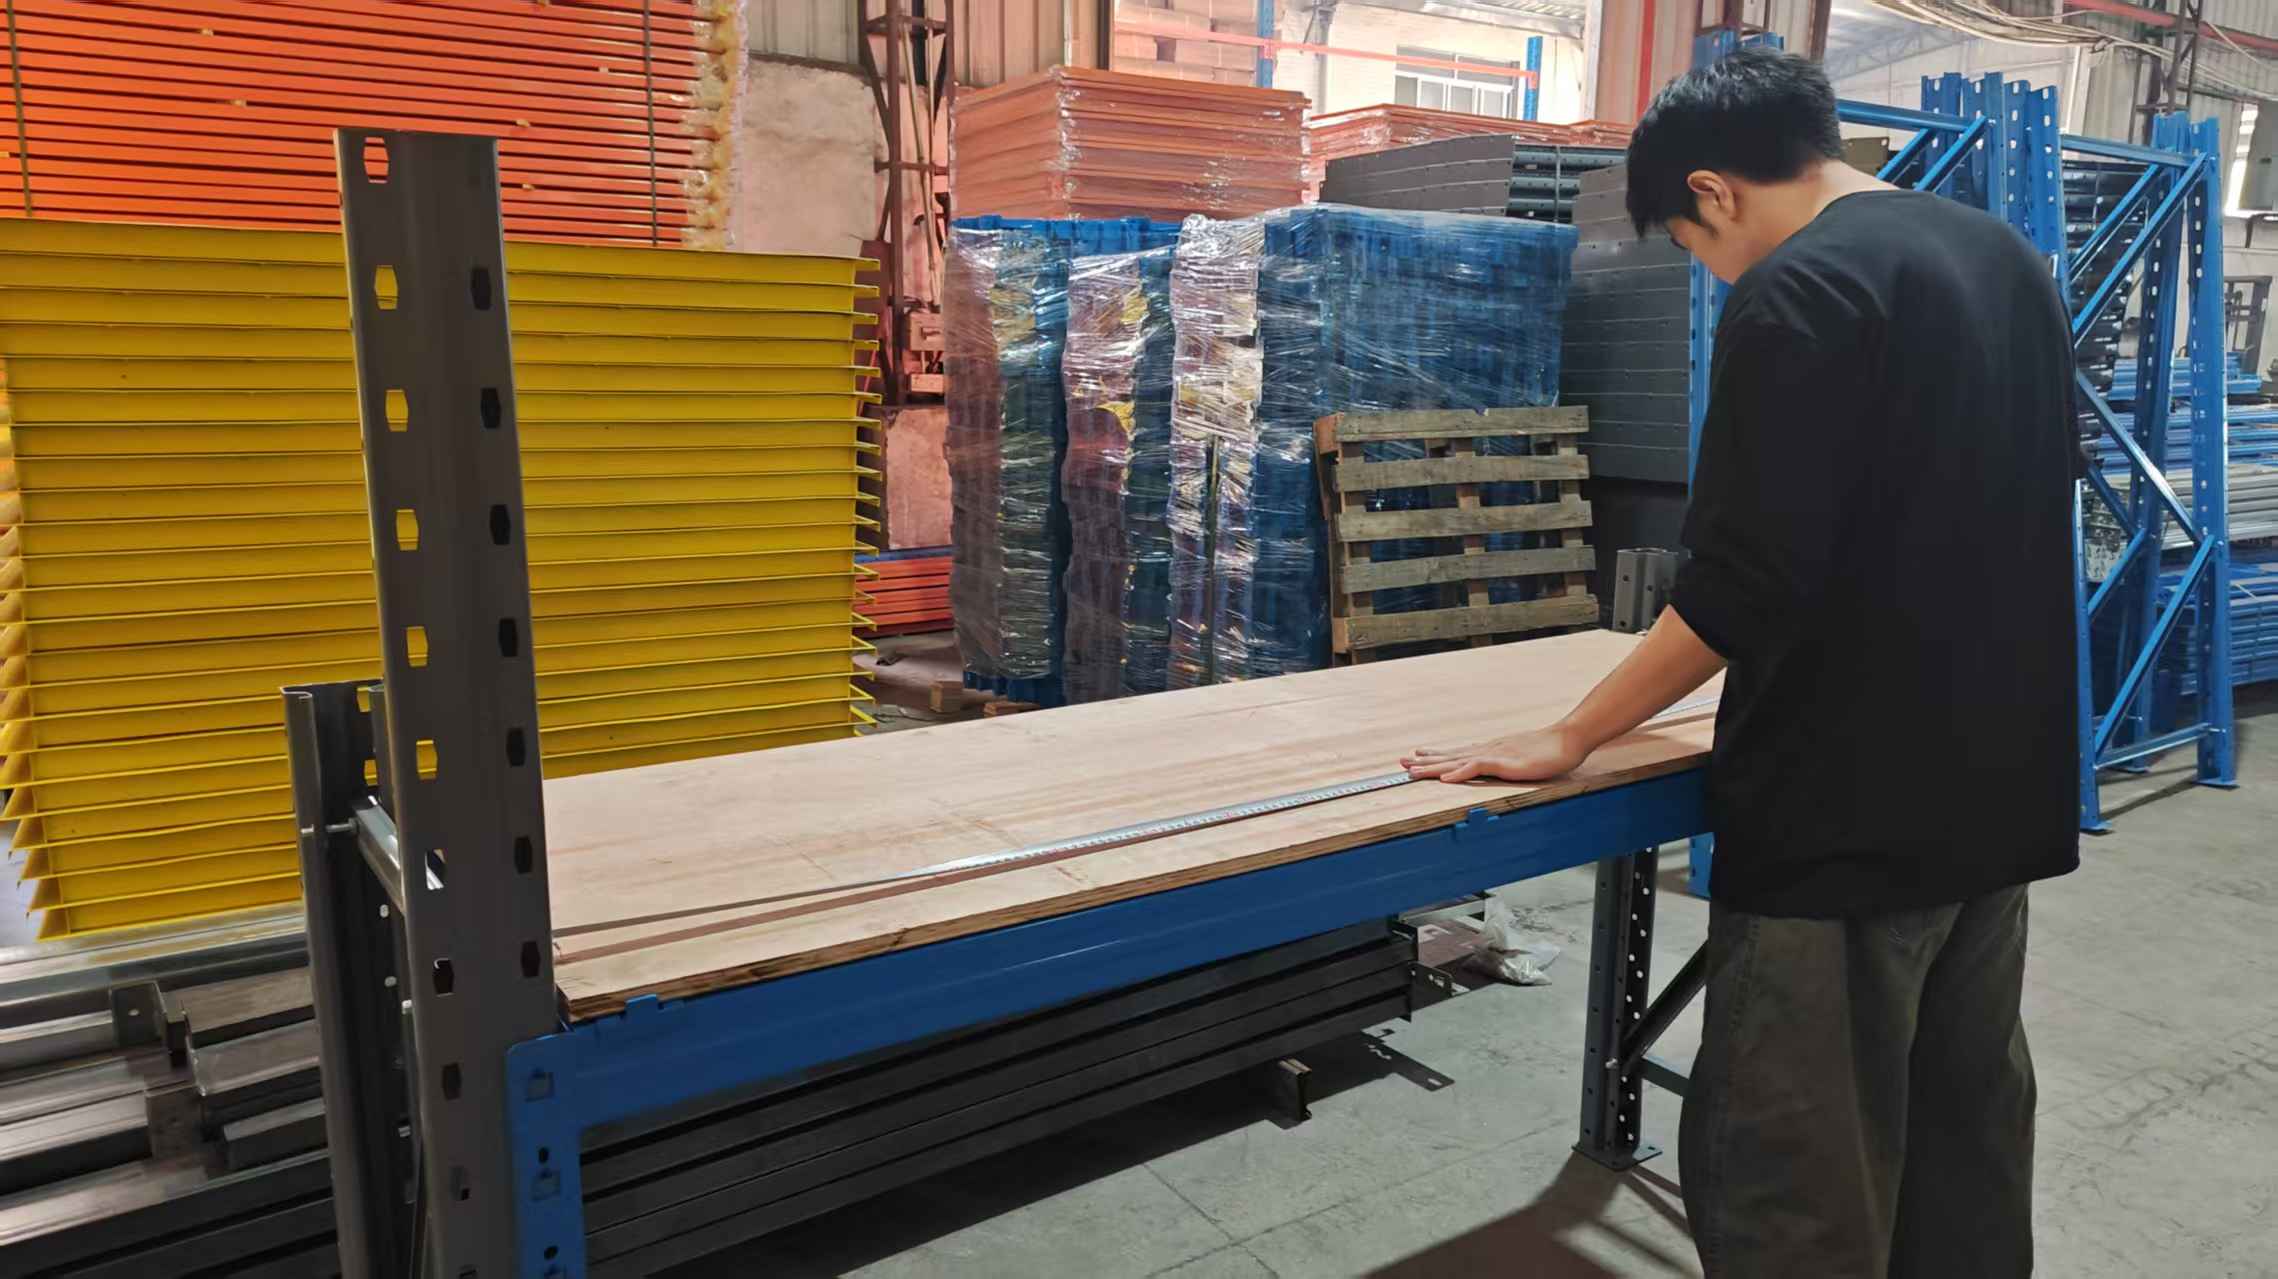
Quality and structural integrity are at the core of our manufacturing philosophy. Backed by a strong network of over 800 supply chain partners, our operation is supported by a dedicated team of 25 Quality Control (QC) specialists. We implement comprehensive non-destructive testing (NDT), load-bearing stress evaluations, and automated ultrasonic weld inspections to ensure that every rack meets stringent international safety standards.
As an export-oriented manufacturer, we primarily serve third-party logistics (3PL) providers, global distributors, and large-scale industrial enterprise clients. Driven by a highly skilled team of 18 R&D engineers, we offer strong OEM/ODM and full custom-tailoring capabilities—from structural engineering and custom dimensions to specialized powder-coating finishes. Continuously advancing warehouse technology, we launched 45 new innovative products last year to support our global partners in optimizing space and efficiency.
Our commitment to innovation is reflected in our advanced production line integration, ensuring that structural tolerances remain within micro-millimeter precision, drastically reducing structural degradation under high-cyclic loads.
Understanding the shifts in modern supply chain ecosystems, vertical warehousing, and the crucial requirement for certified high-density storage frameworks.
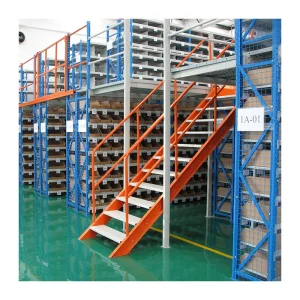
With global e-commerce volumes scaling exponentially, third-party logistics providers require ultra-durable pallet racking systems that support high-turnover picking, multi-tier mezzanine integration, and seamless automated guided vehicle (AGV) pathways.
International buyers are increasingly stringent regarding seismic resistance, RMI/FEM compliance, and rigorous load-bearing certification. Safety margins are no longer optional; they are the baseline for enterprise asset protection.
Modern warehouses demand flexible, boltless, and modular designs that can scale or reconfigure rapidly without extensive downtime, ensuring maximum return on capital expenditure (CapEx).
How advanced smart manufacturing, automated robotics, and precision engineering give our global partners a decisive competitive cost and quality advantage.
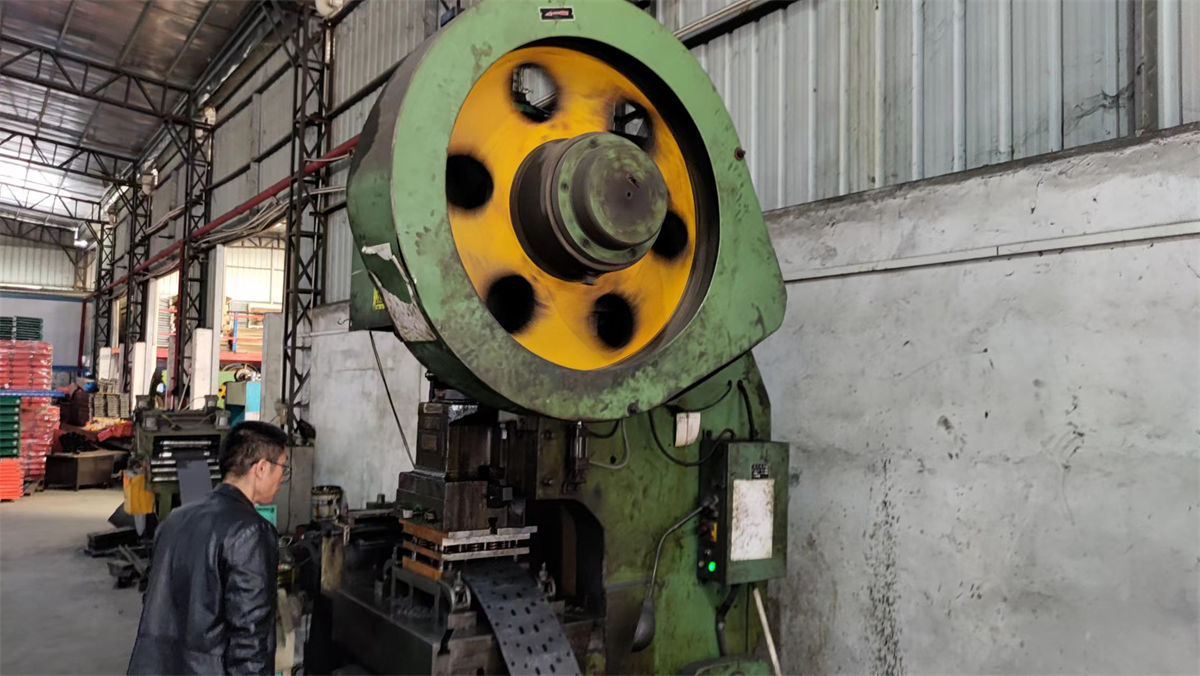
Utilizing high-speed computerized rolling and punching lines to ensure flawless profile consistency and structural load-bearing symmetry.
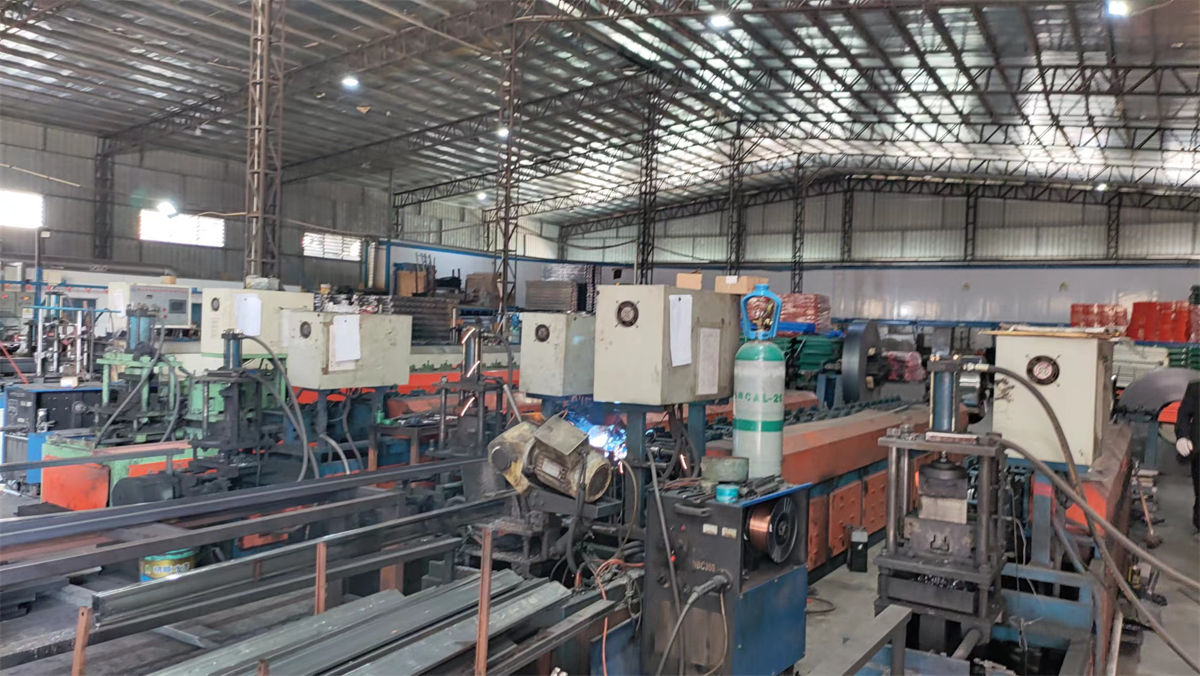
State-of-the-art robotic welding coupled with electrostatic powder-coating lines guarantees long-term corrosion resistance and pristine aesthetic durability.
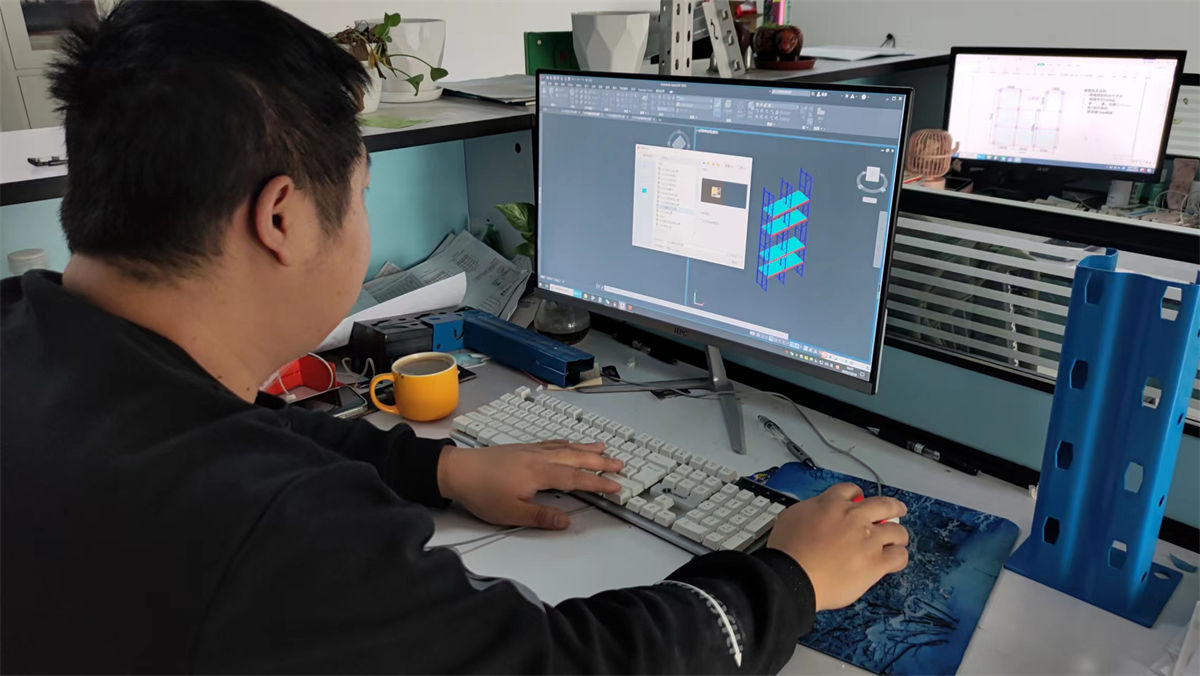
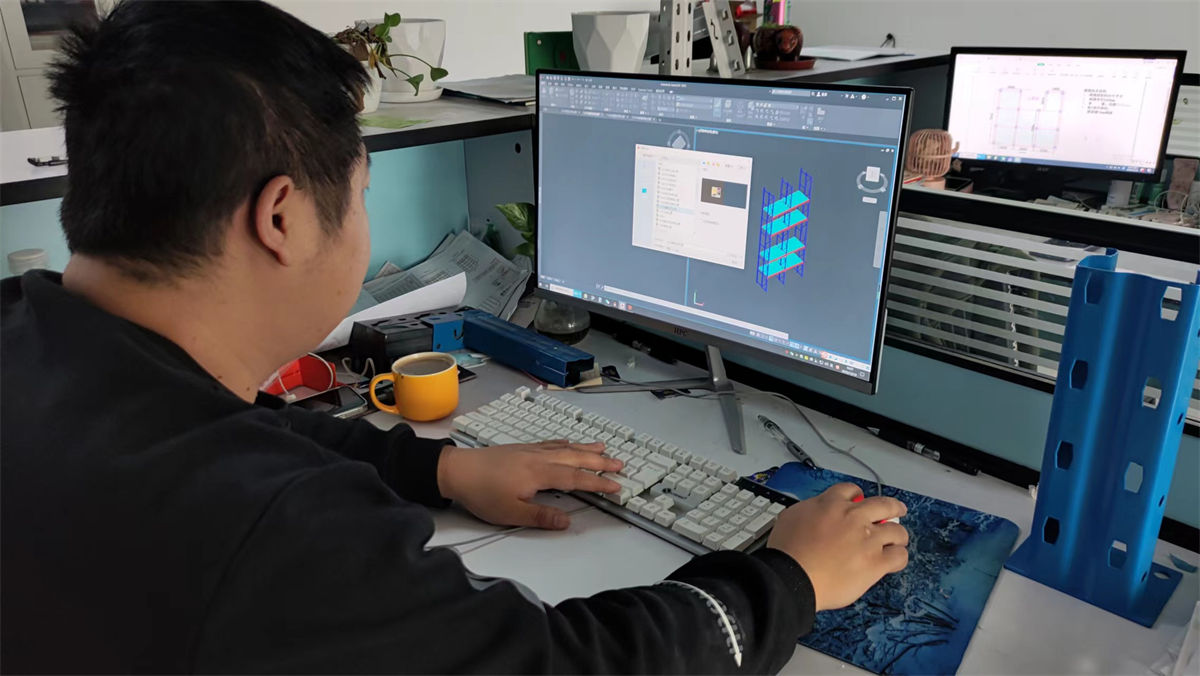
In-house CAD simulation software and digital prototyping allow custom architectural adaptations tested against extreme stress tolerances.
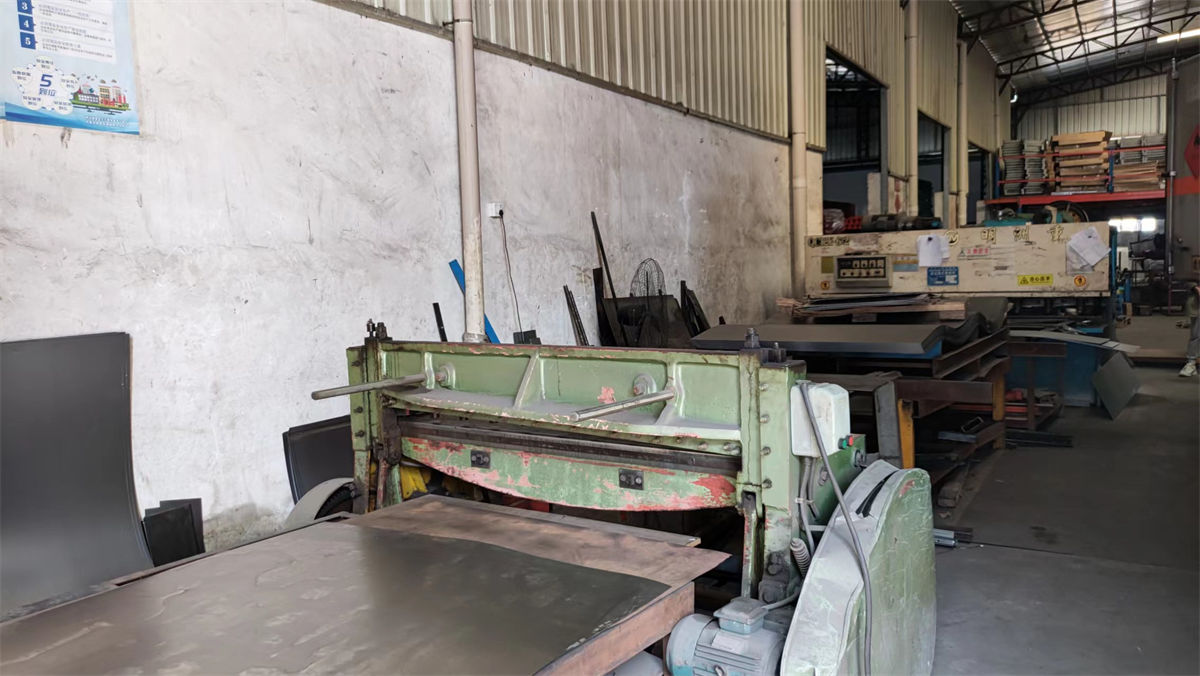
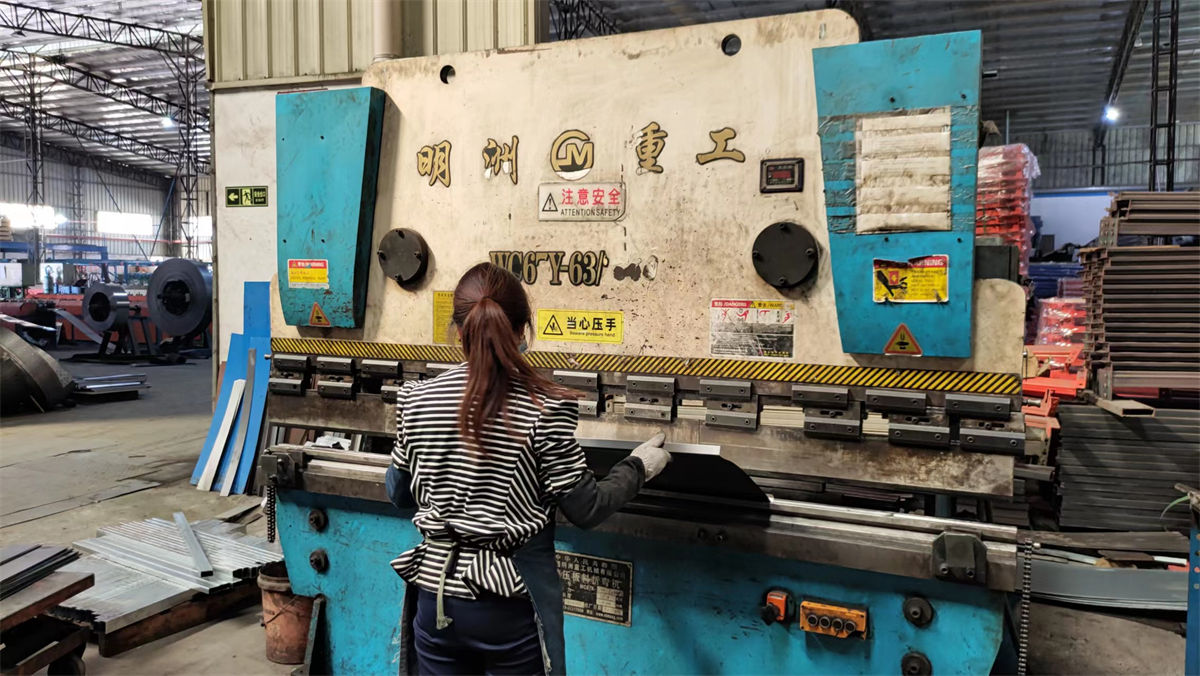
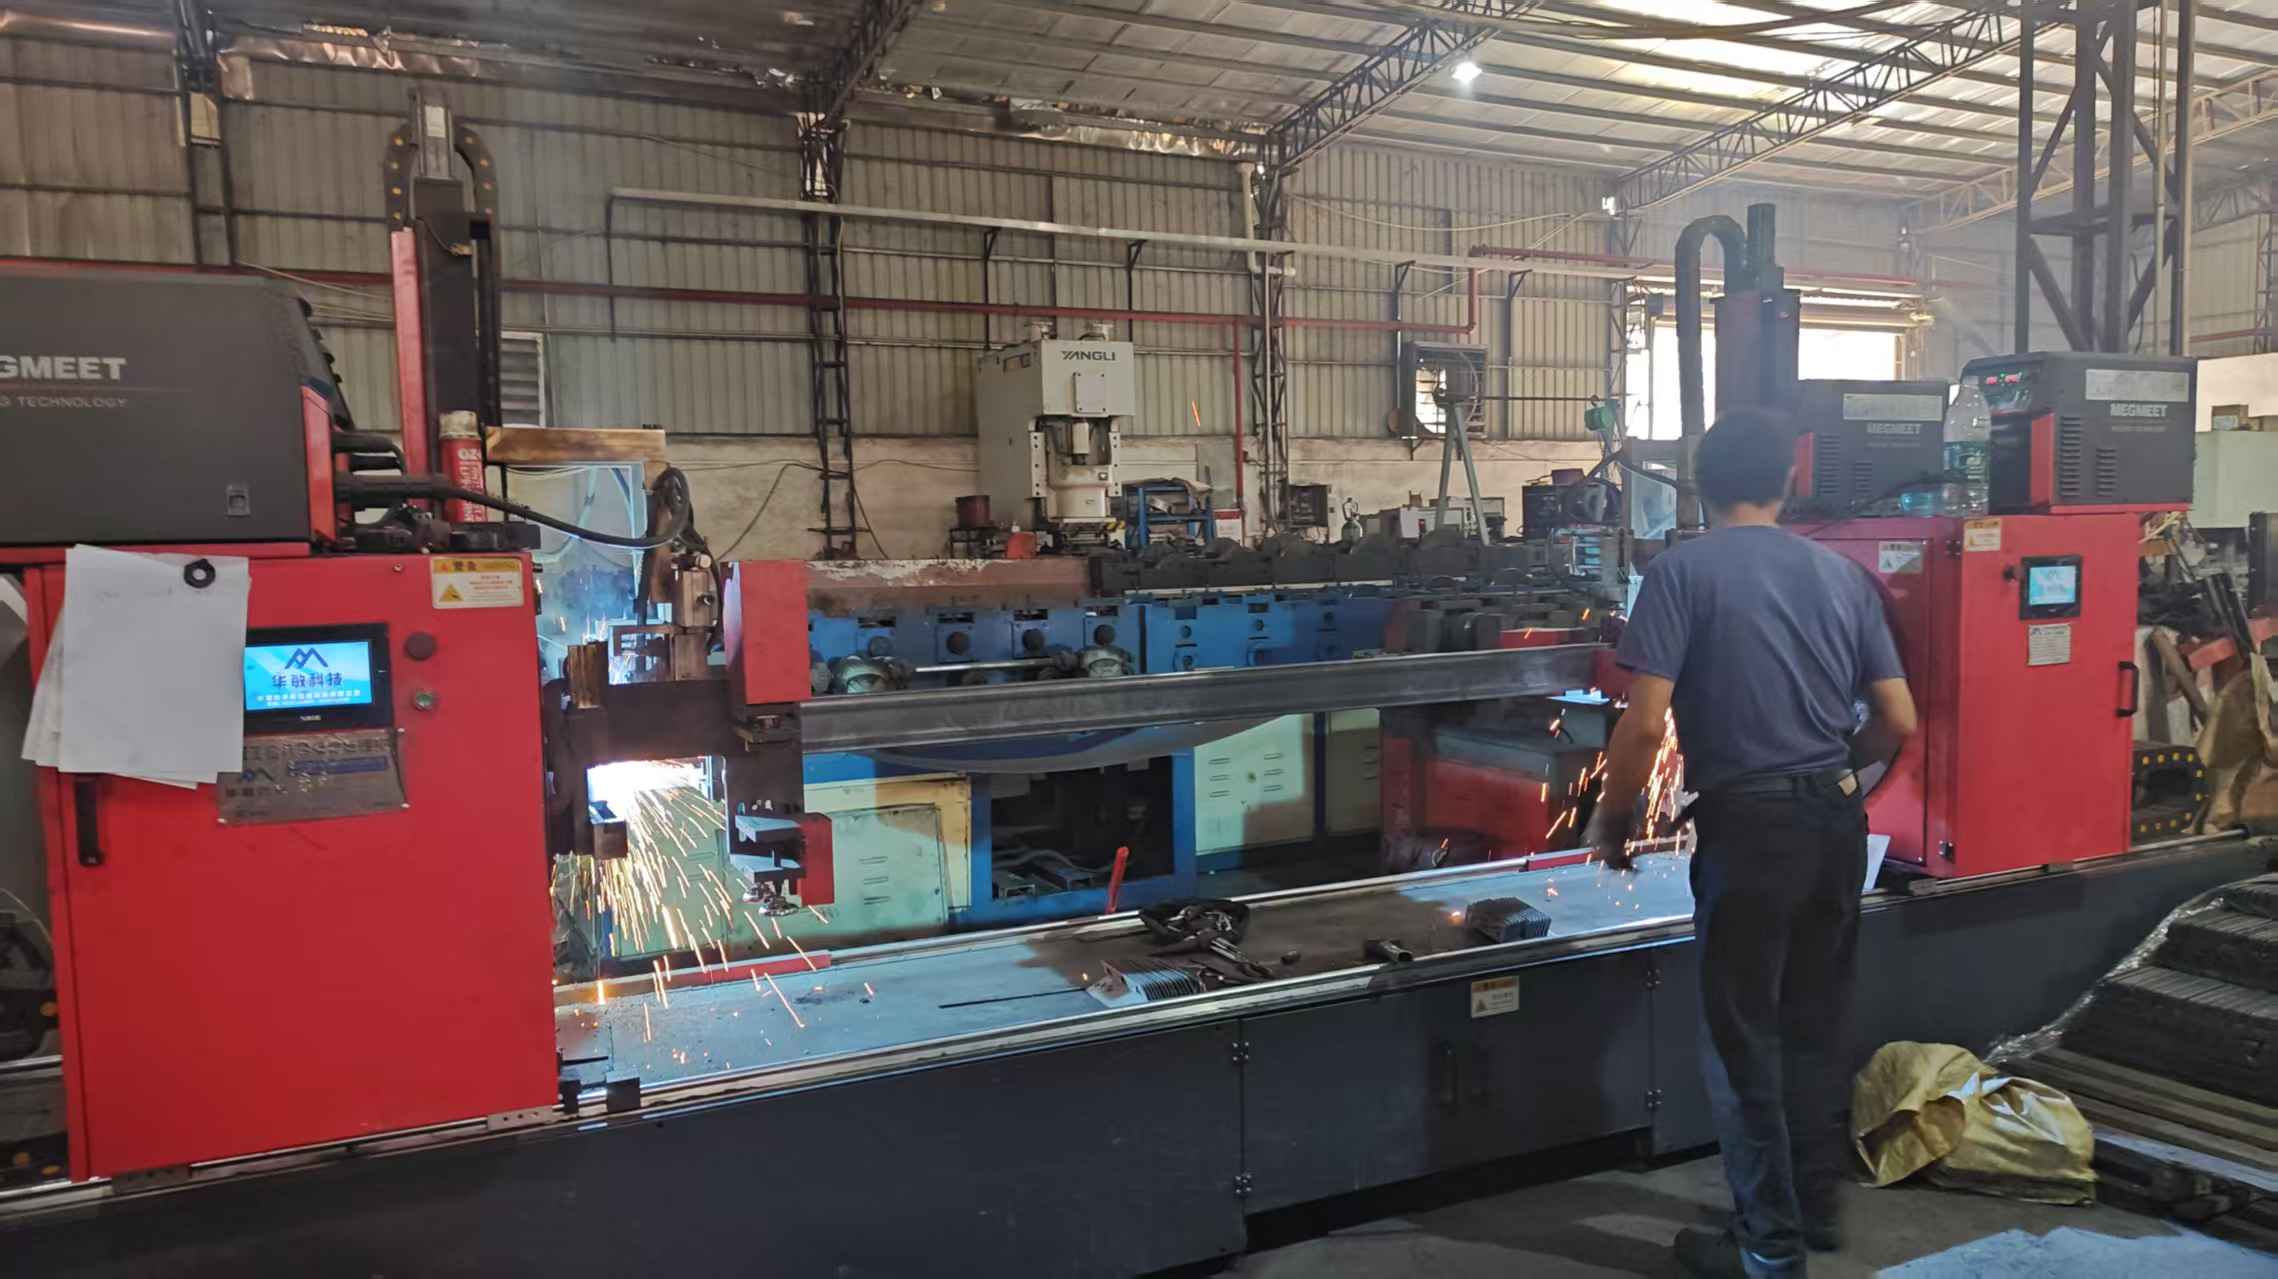
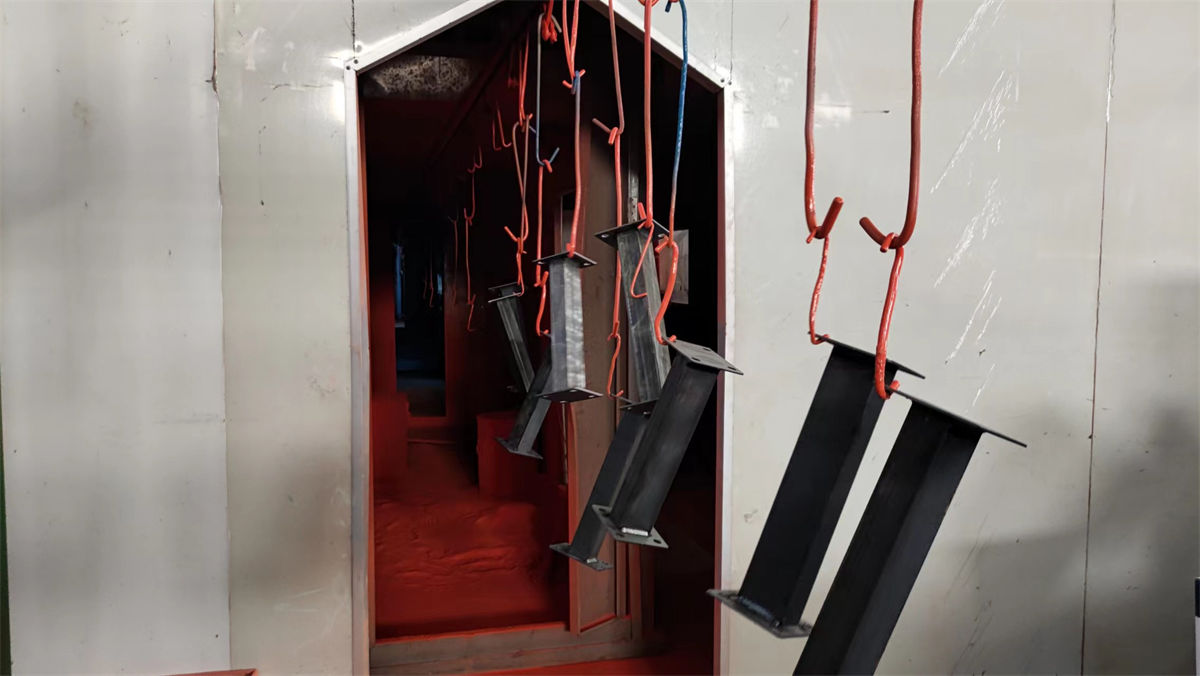
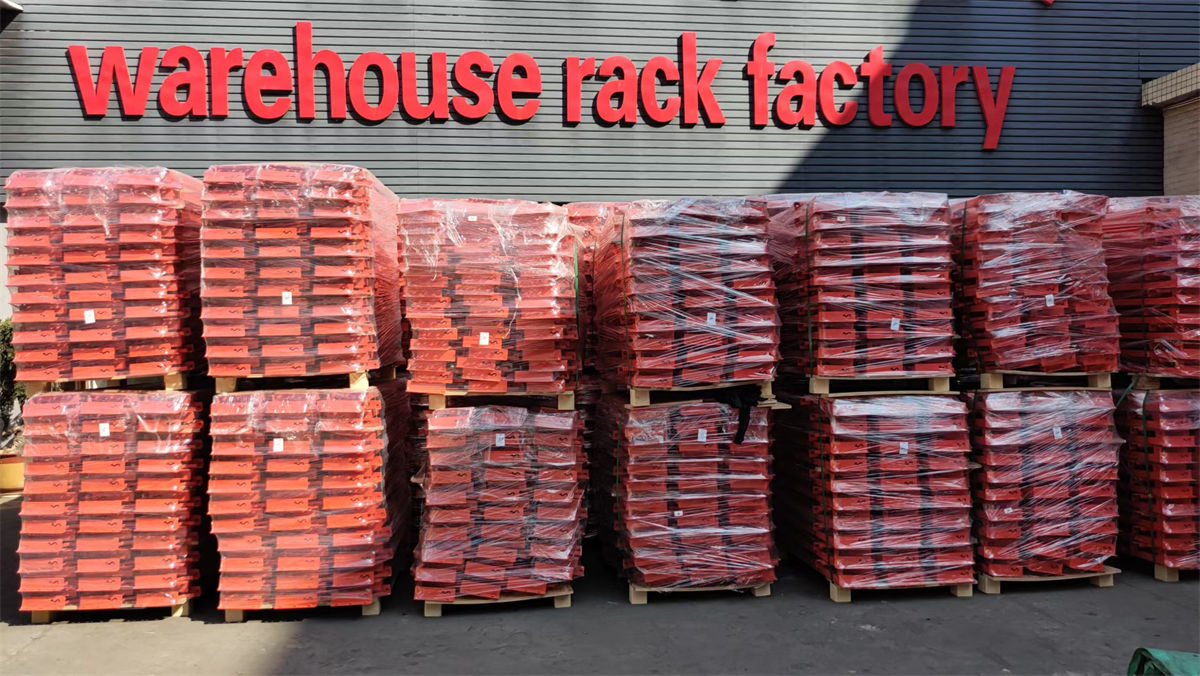
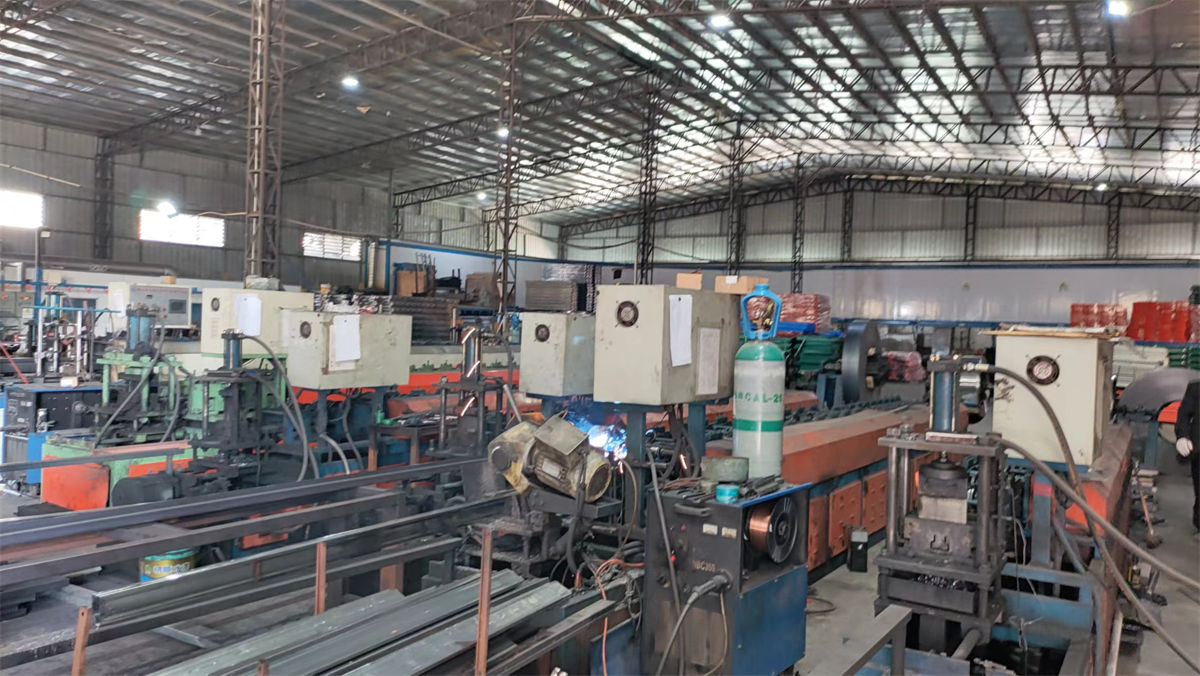
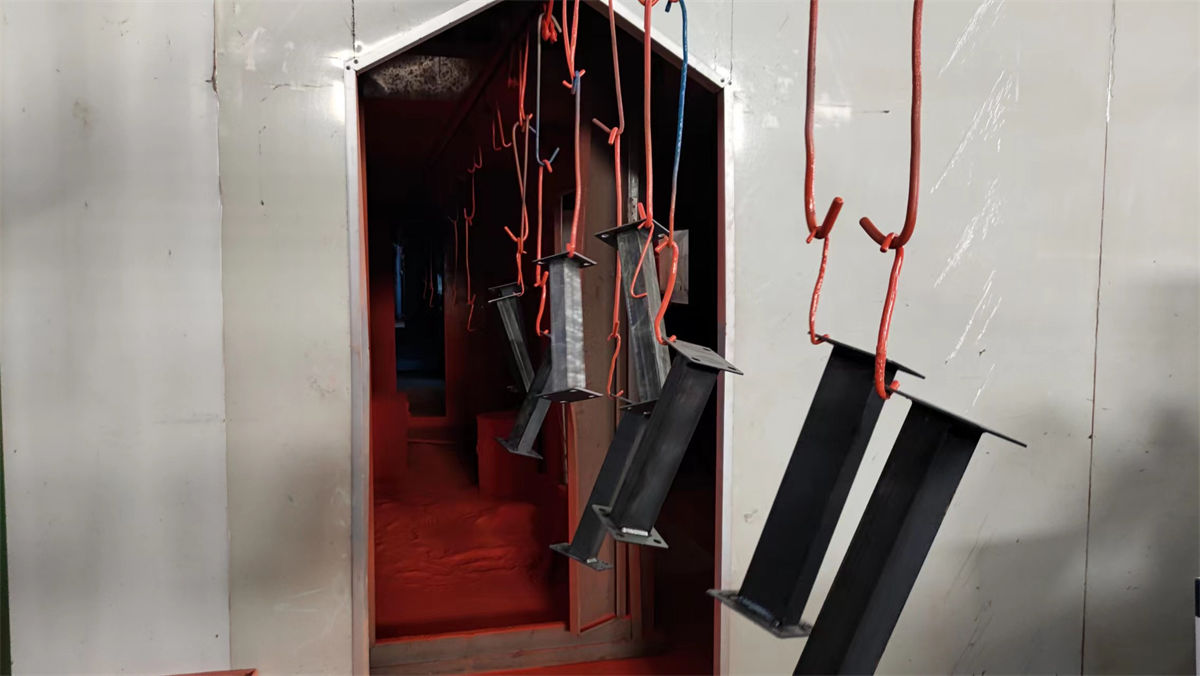
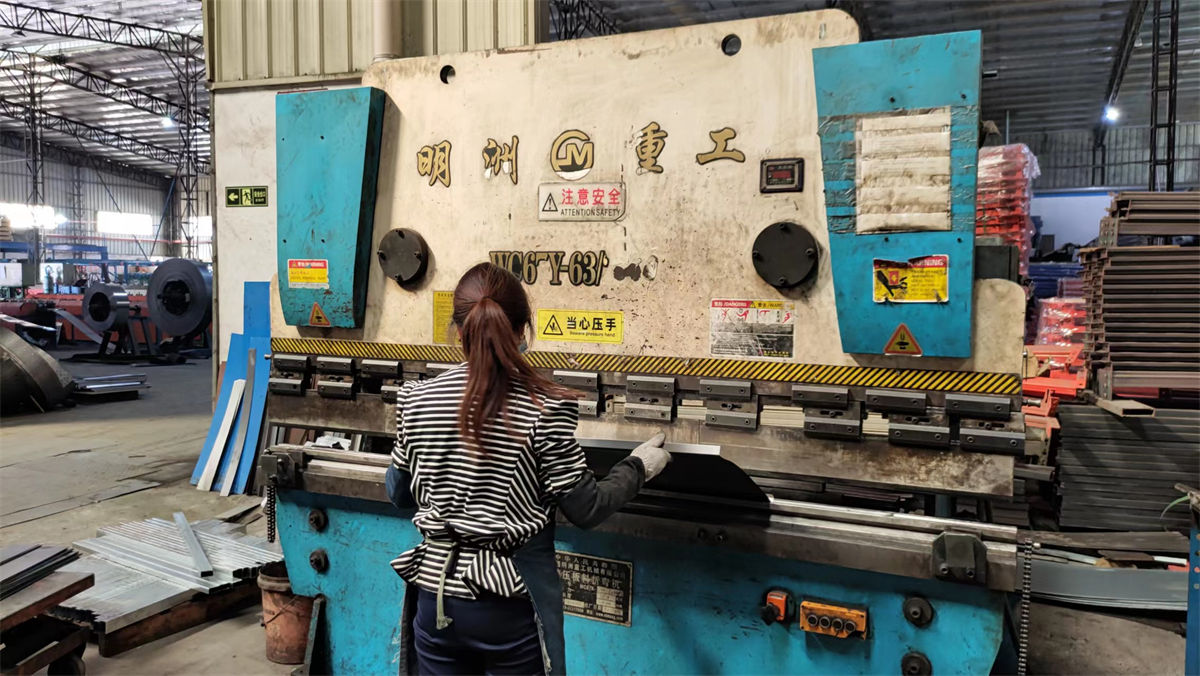
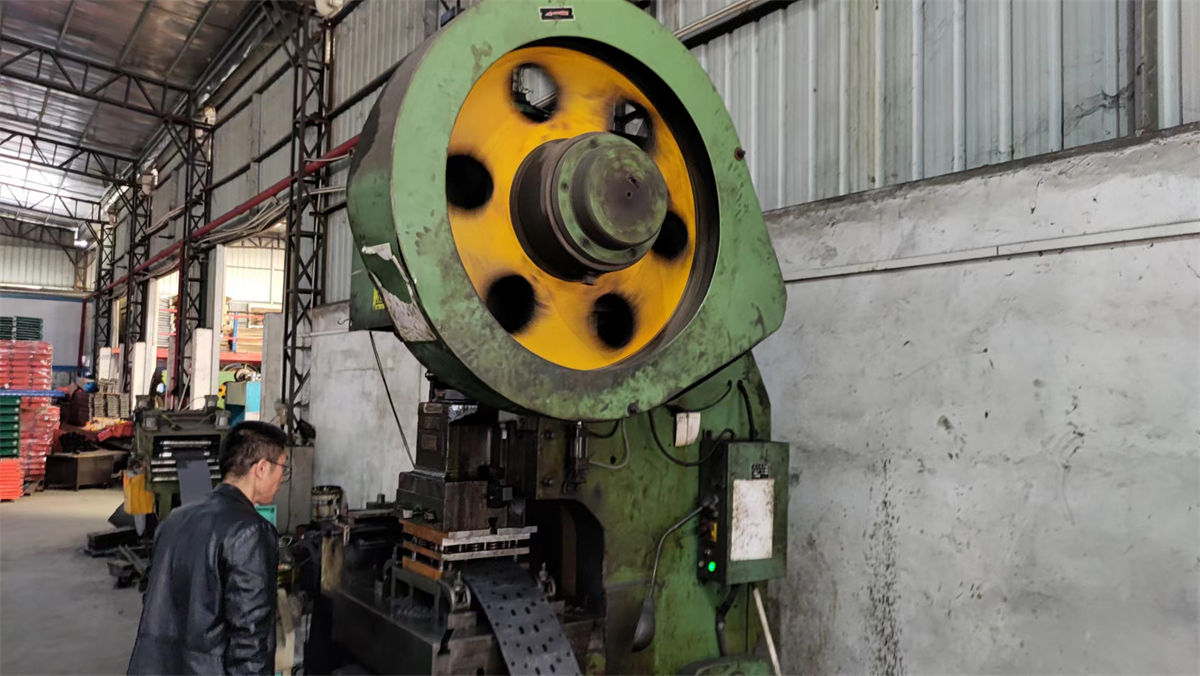
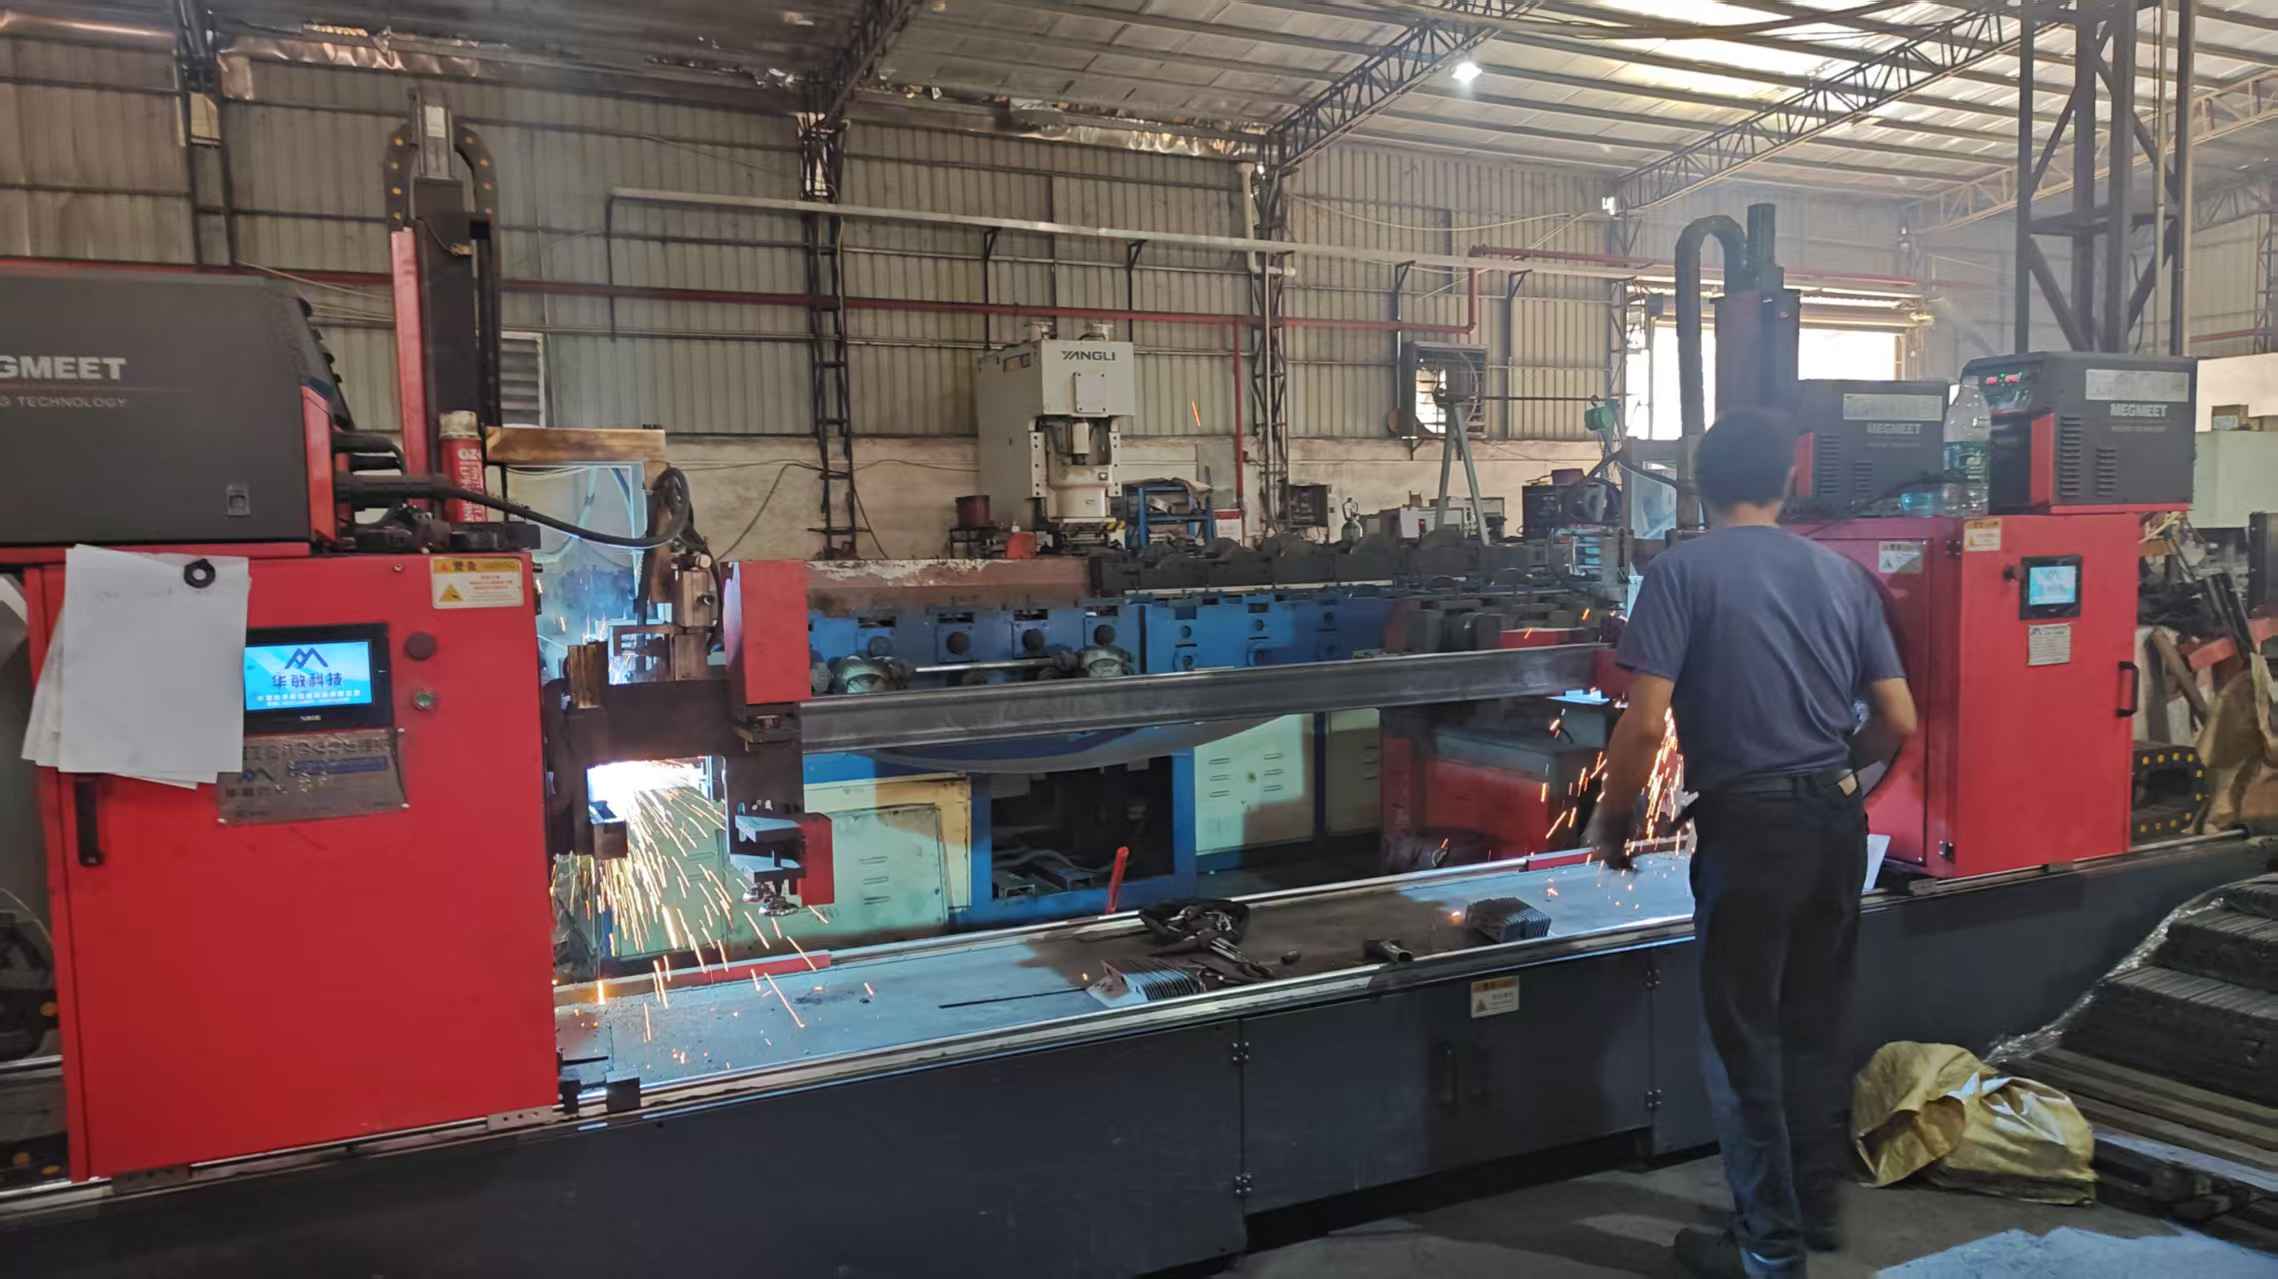
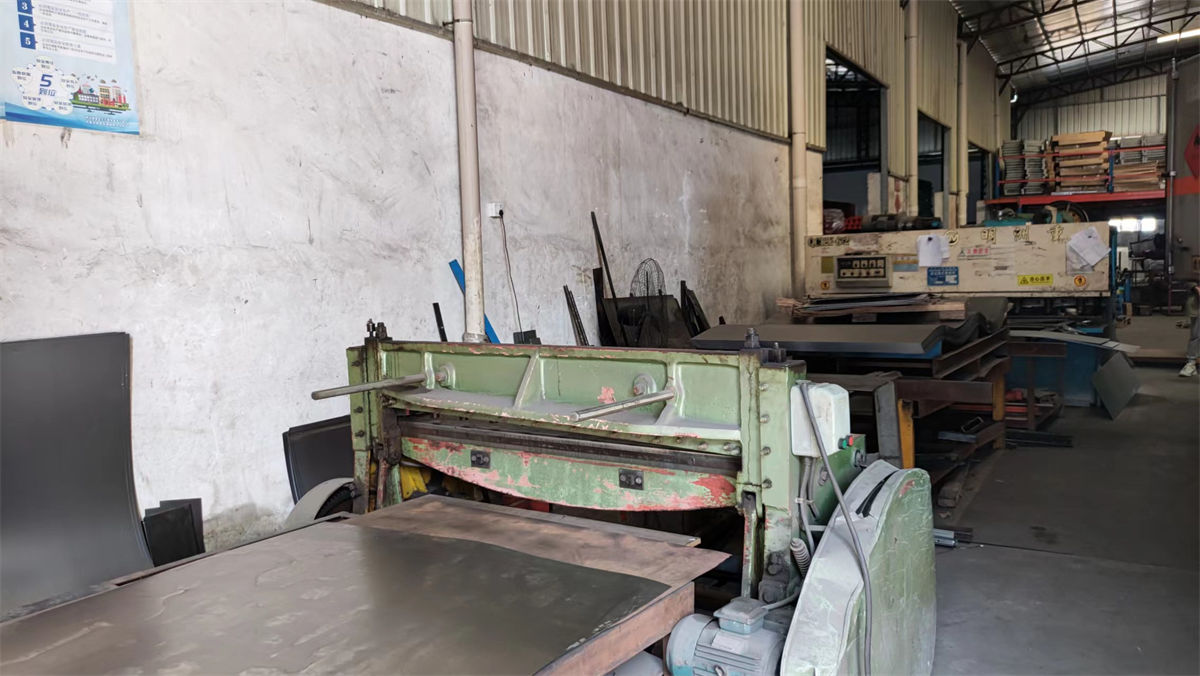
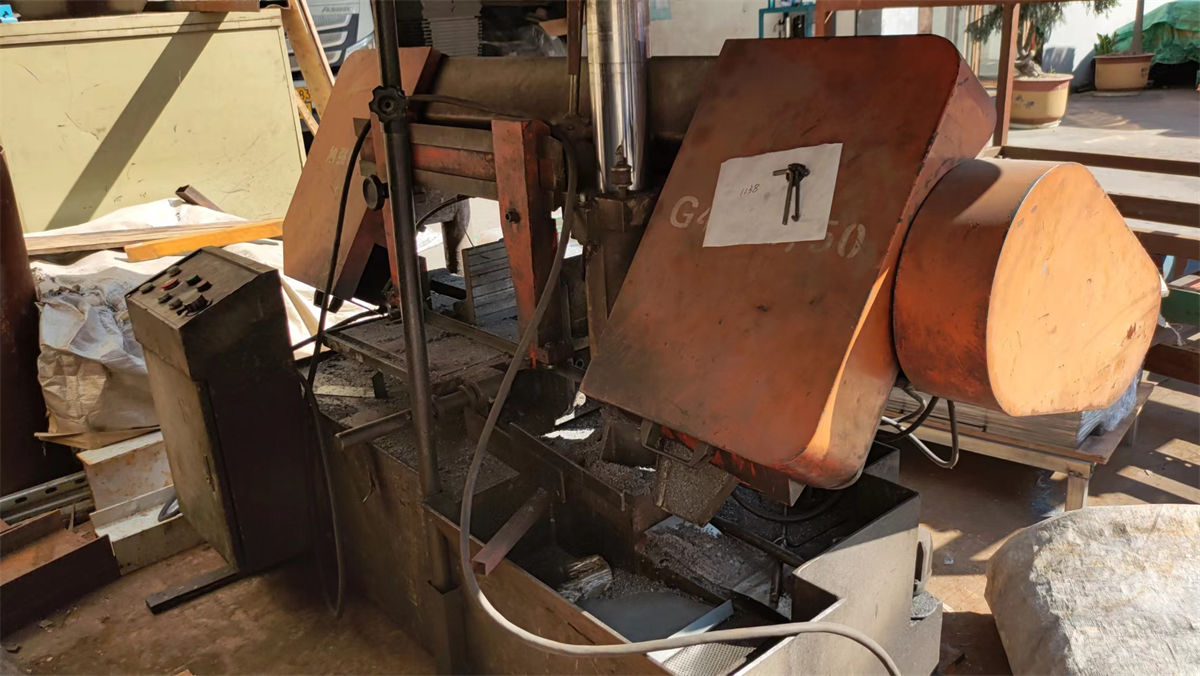
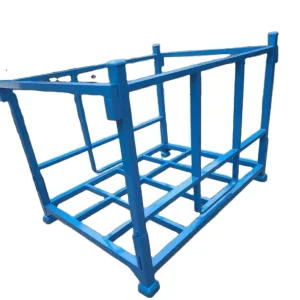
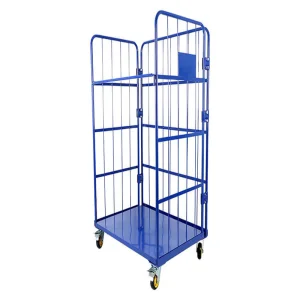
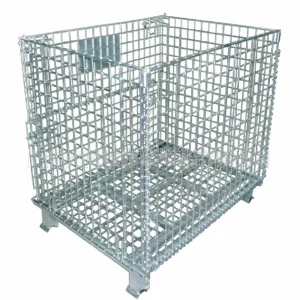
Discover our heavy-duty roll containers, stackable wire mesh cages, and automated radio shuttle systems engineered for high-efficiency fulfillment operations.
Expert answers regarding global shipping, custom engineering, and structural certifications for industrial pallet racking.
With over 14 years of dedicated manufacturing experience, a 35,000+ sqm advanced facility, 25 specialized QC engineers, and robust OEM/ODM capabilities, we deliver certified high-load industrial racking systems globally with strict adherence to international safety standards.
Yes. Our in-house team of 18 R&D engineers provides tailored structural design services, adjusting upright heights, beam lengths, steel thickness, and powder-coating finishes to match your exact spatial and weight capacity requirements.
Our products undergo rigorous non-destructive testing (NDT), load-bearing stress evaluations, and automated ultrasonic weld inspections, ensuring compliance with major global industrial racking standards.
Thanks to our automated rolling and punching production lines and a strong network of over 800 supply chain partners, we maintain high production efficiency, typically fulfilling standard container export orders within 20 to 30 days.
 Xinmiao Racking