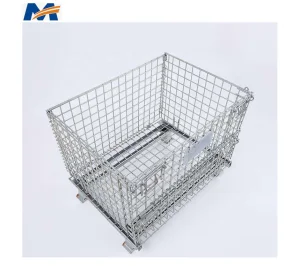
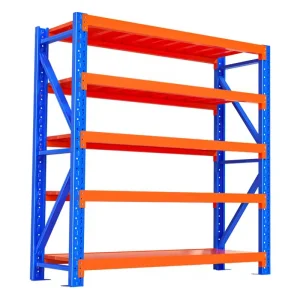
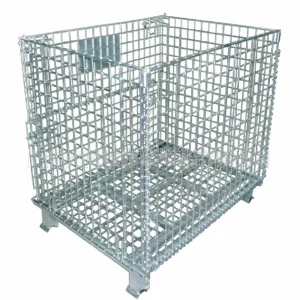
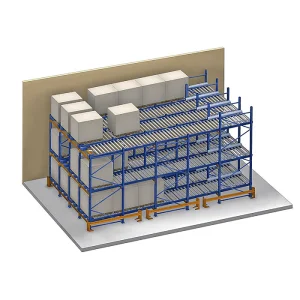
Explore our engineered pallet racks, mesh containers, and boltless shelving systems designed for maximum industrial density.

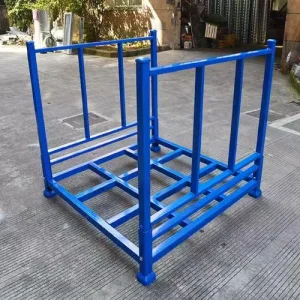
A Comprehensive Industry Whitepaper on Global Supply Chain Evolution and Chinese Manufacturing Leadership.
In the contemporary global landscape, Warehouse Management and industrial logistics infrastructure serve as the ultimate backbone of international commerce, e-commerce fulfillment, and third-party logistics (3PL) operations. As global supply chains face unprecedented demands for rapid fulfillment, high SKU density, and cost optimization, enterprises across North America, Europe, Southeast Asia, and the Middle East are rapidly upgrading their storage architecture. From traditional selective pallet racks to automated storage and retrieval systems (AS/RS), structural integrity, spatial efficiency, and safety compliance have become non-negotiable standards for modern industrial facilities.
China has emerged indisputably as the global epicenter for warehouse management equipment manufacturing and wholesale supply. Leveraging complete industrial clusters, advanced metallurgical processing, and highly refined automated production lines, Chinese manufacturers deliver structural steel solutions—such as heavy-duty Q235B cold-rolled steel racks, mezzanine flooring systems, and wire mesh containers—that meet or exceed stringent international standards including RMI, FEM, and CE.
Established in 2015, Ningbo Xinmiao Storage Equipment Co., Ltd. (widely recognized through our brand Mracking) represents the pinnacle of Chinese manufacturing excellence. Spanning a modern manufacturing facility of over 35,000 square meters, we have dedicated over 14 years to the industry, providing robust and reliable storage solutions to global enterprise clients. With 8 years of direct export experience, our products are trusted in key markets across North America, Europe, Southeast Asia, and the Middle East, generating an annual export revenue exceeding $18 million.
How rigorous engineering and dedicated testing ensure maximum structural safety across all global deployments.
Quality and structural integrity are at the core of our manufacturing philosophy. Backed by a strong network of over 800 supply chain partners, our operation is supported by a dedicated team of 25 Quality Control (QC) specialists. We implement comprehensive non-destructive testing (NDT), load-bearing stress evaluations, and automated ultrasonic weld inspections to ensure that every rack meets stringent international safety standards.
As an export-oriented manufacturer, we primarily serve third-party logistics (3PL) providers, global distributors, and large-scale industrial enterprise clients. Driven by a highly skilled team of 18 R&D engineers, we offer strong OEM/ODM and full custom-tailoring capabilities—from structural engineering and custom dimensions to specialized powder-coating finishes. Continuously advancing warehouse technology, we launched 45 new innovative products last year to support our global partners in optimizing space and efficiency.
Precision engineering executed through state-of-the-art machinery, rigorous inspection, and advanced CAD design systems.
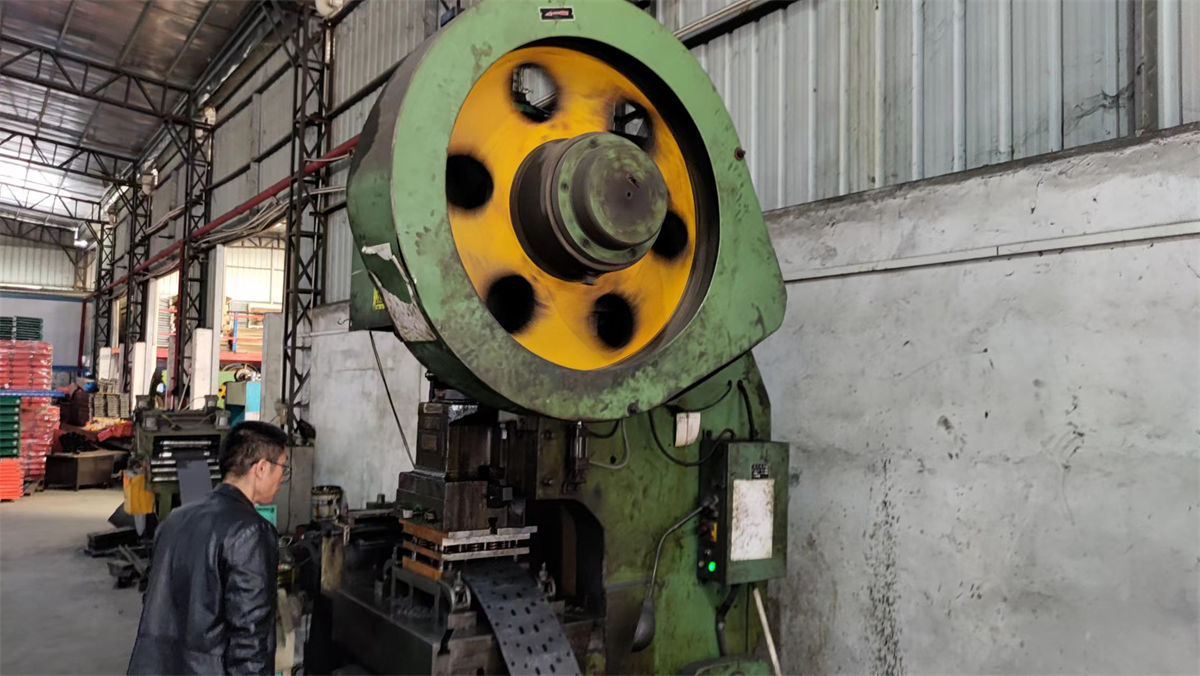
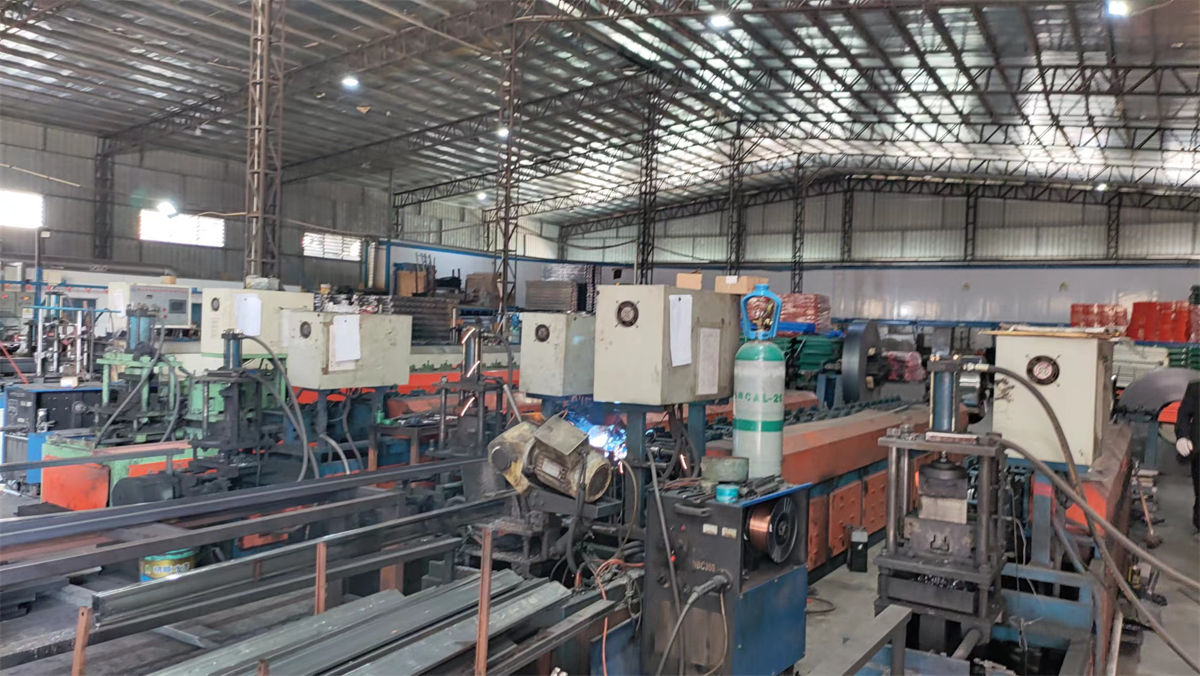
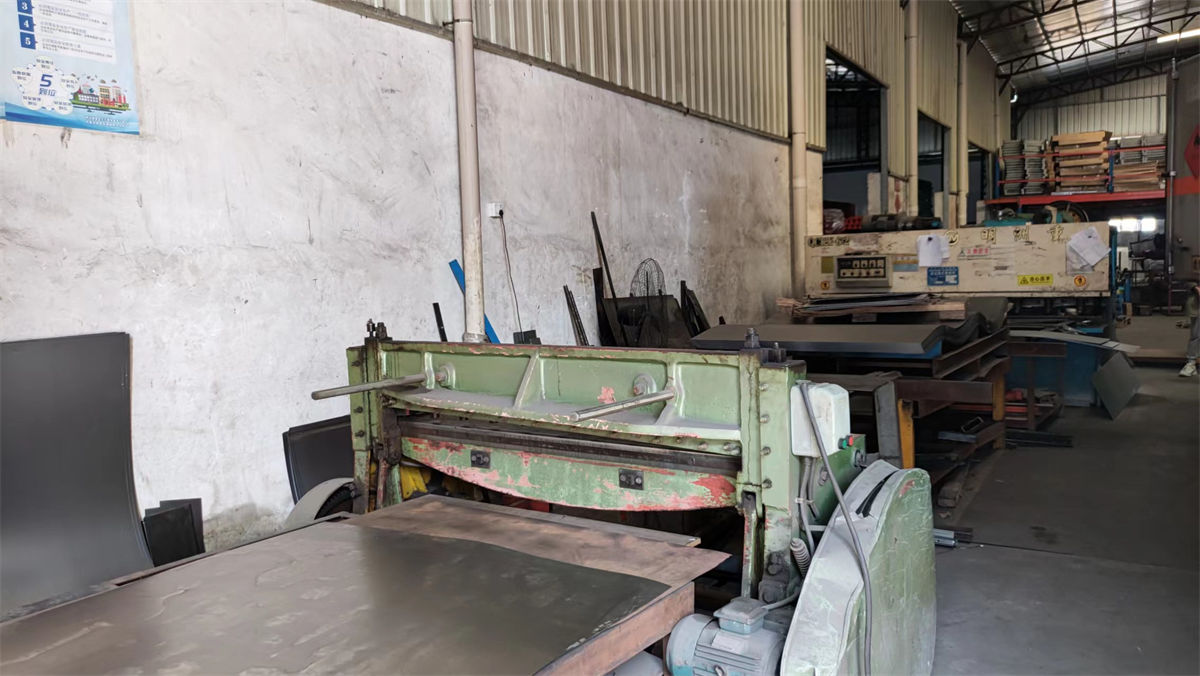
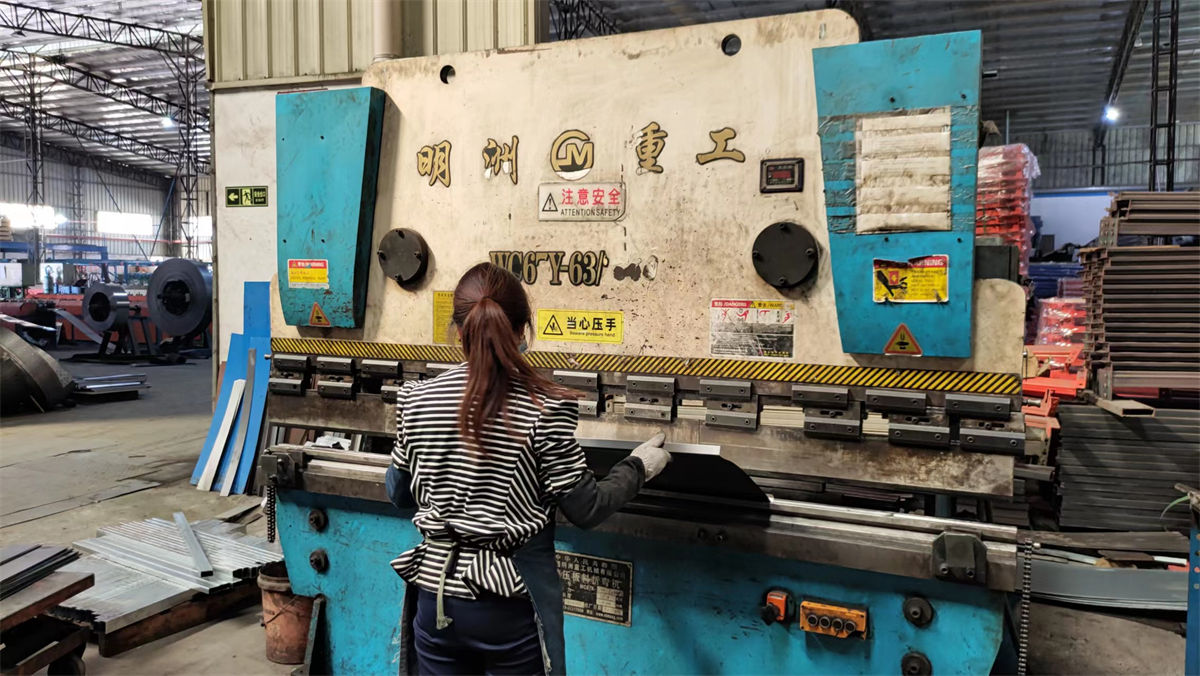
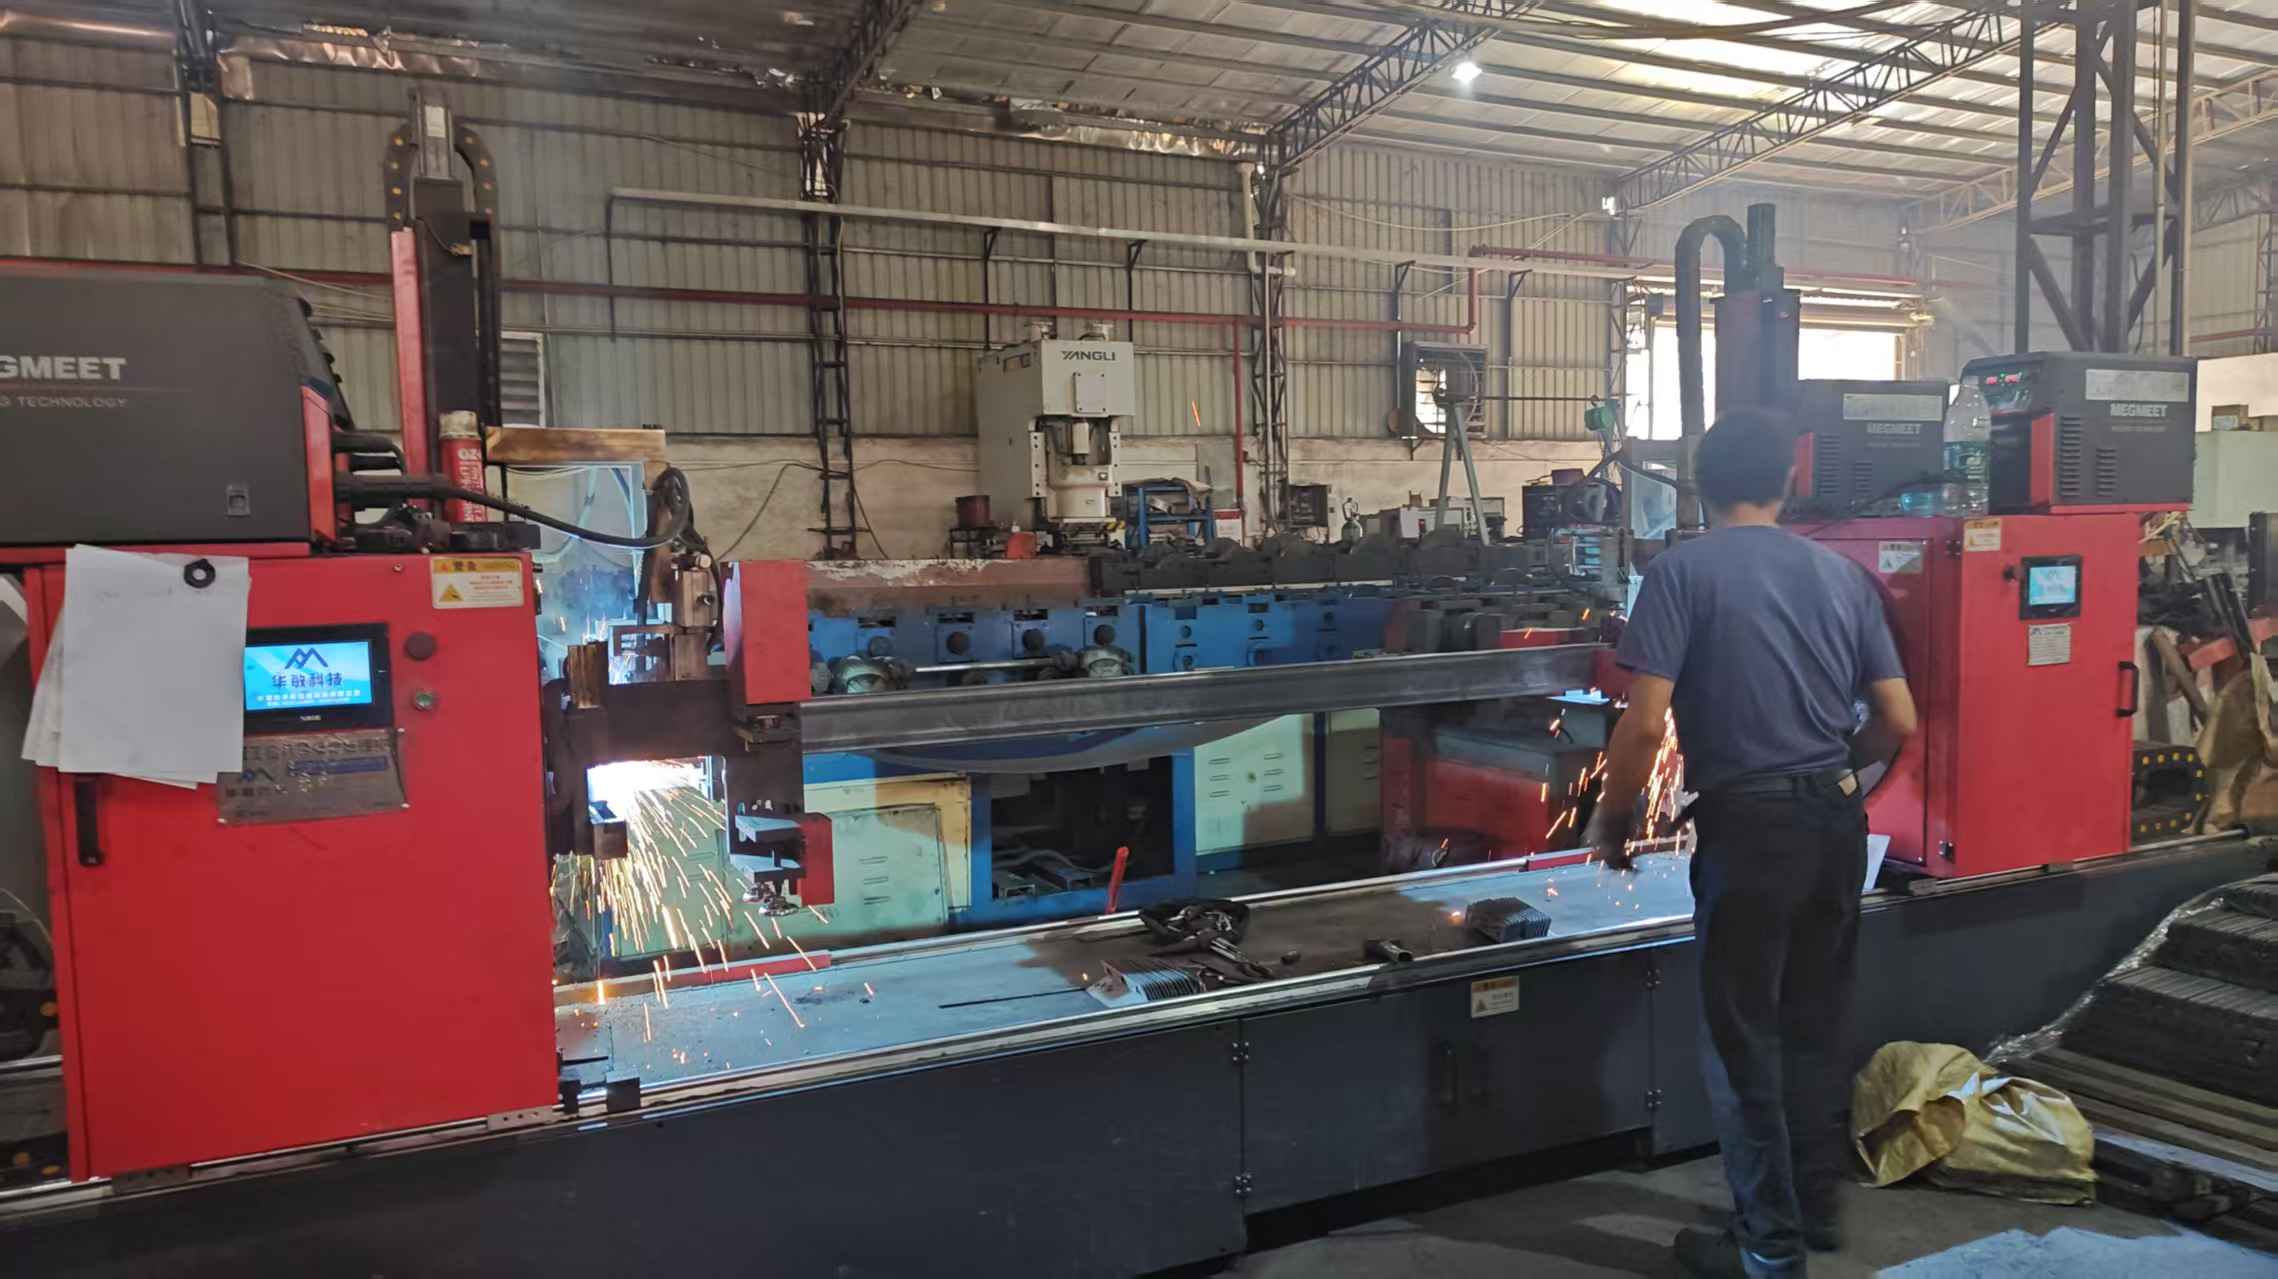
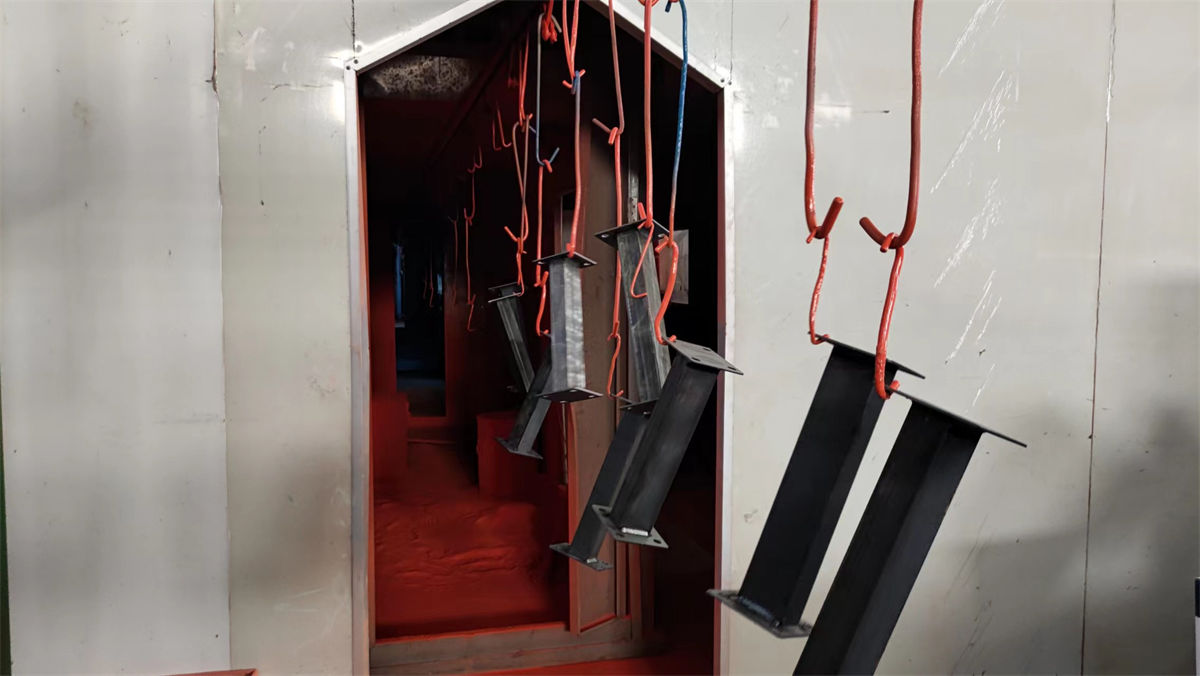
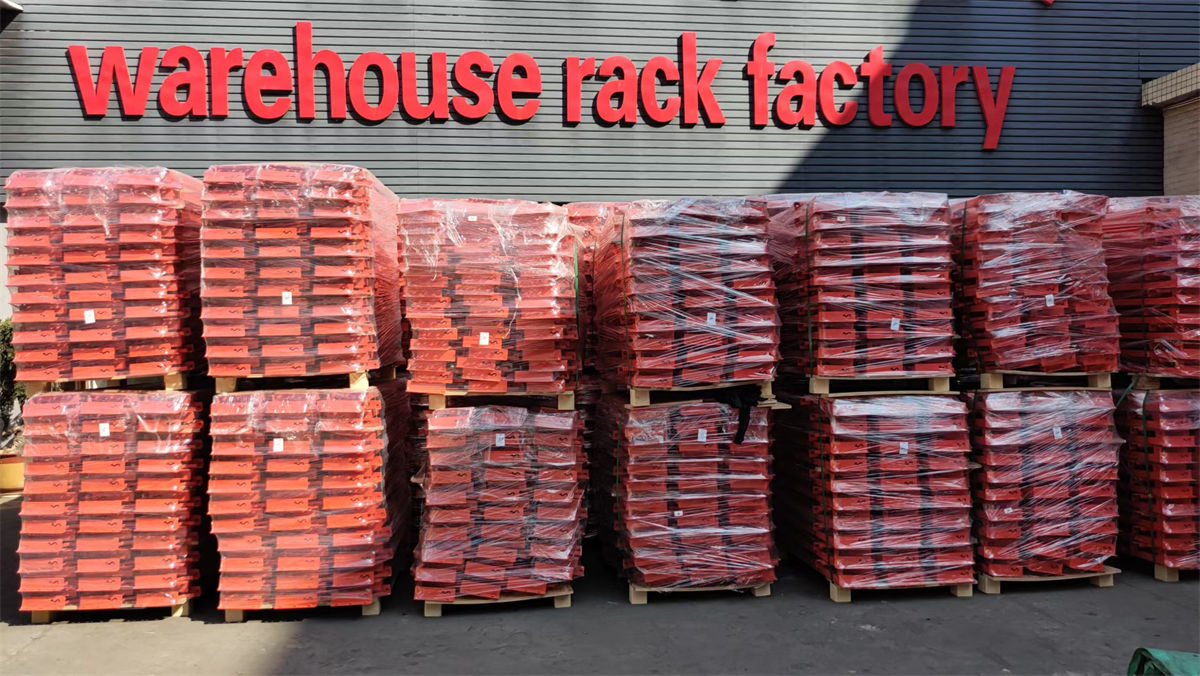
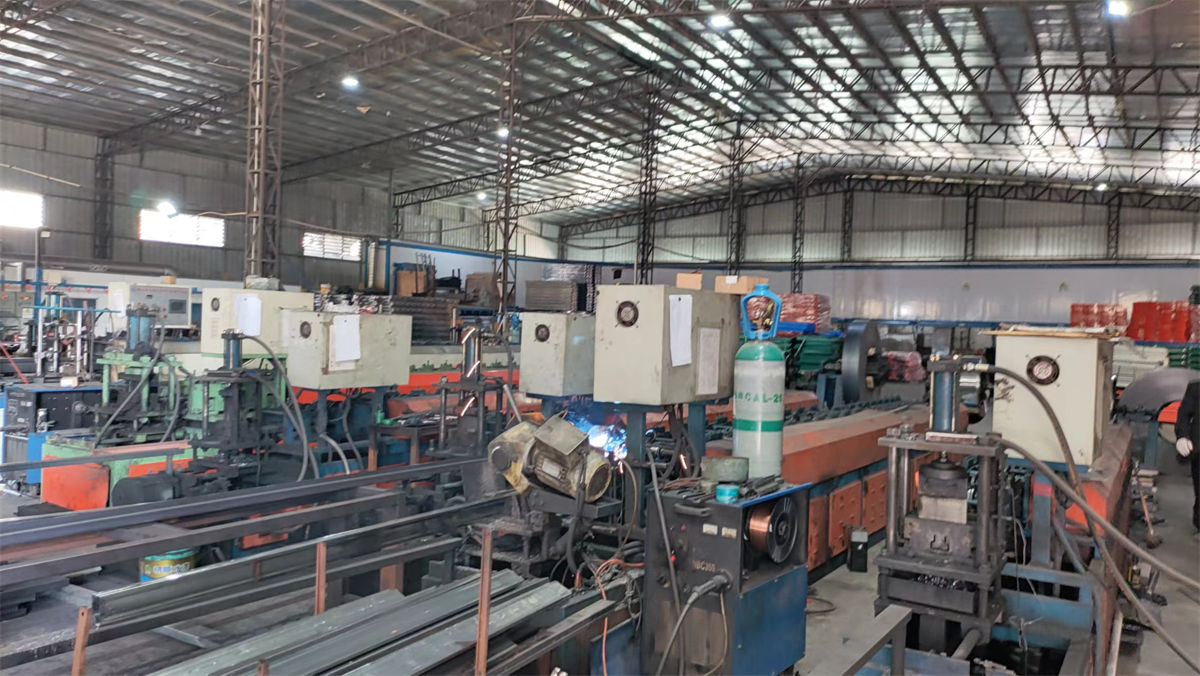
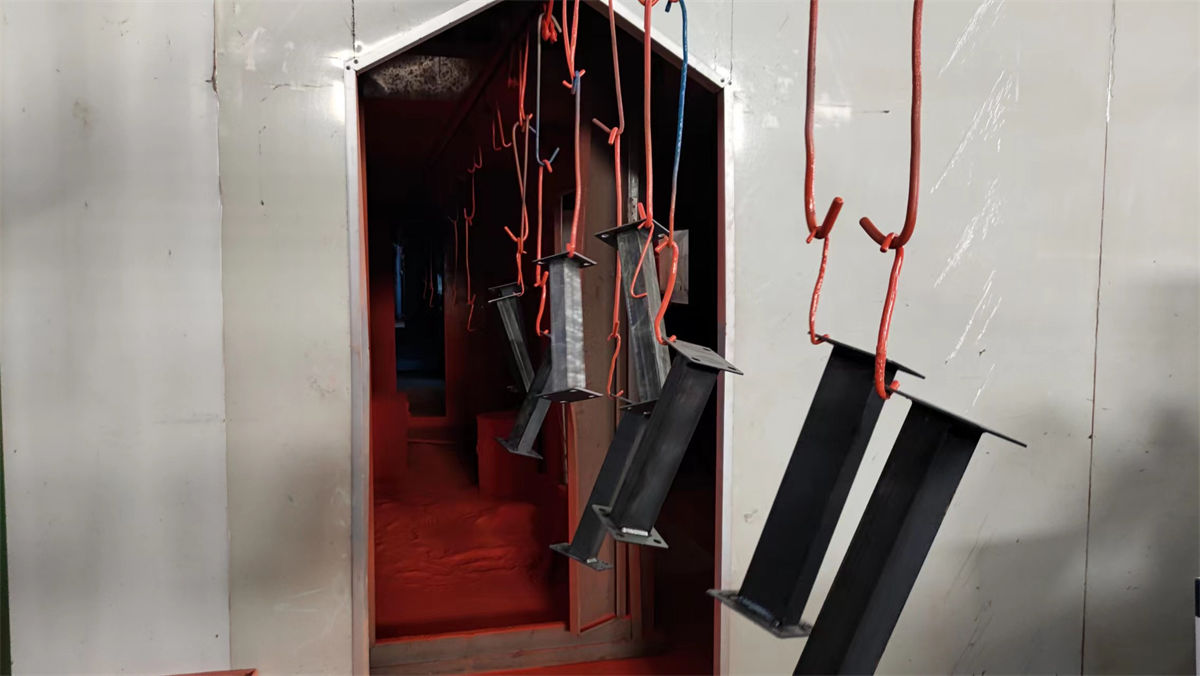
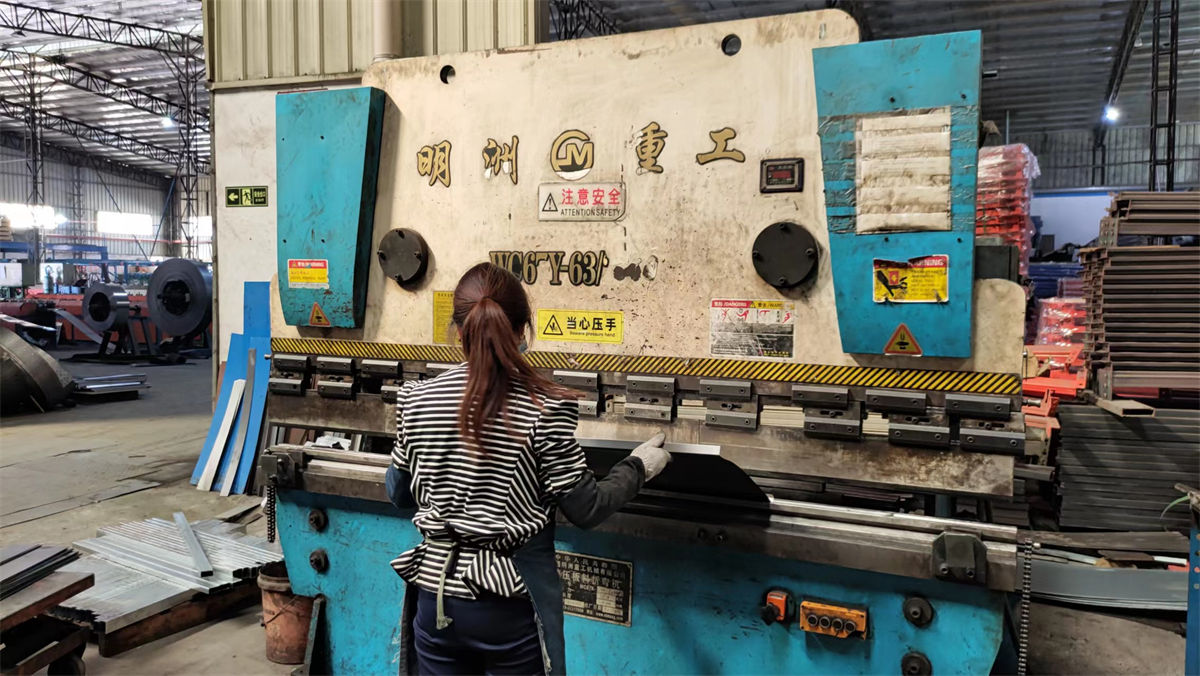
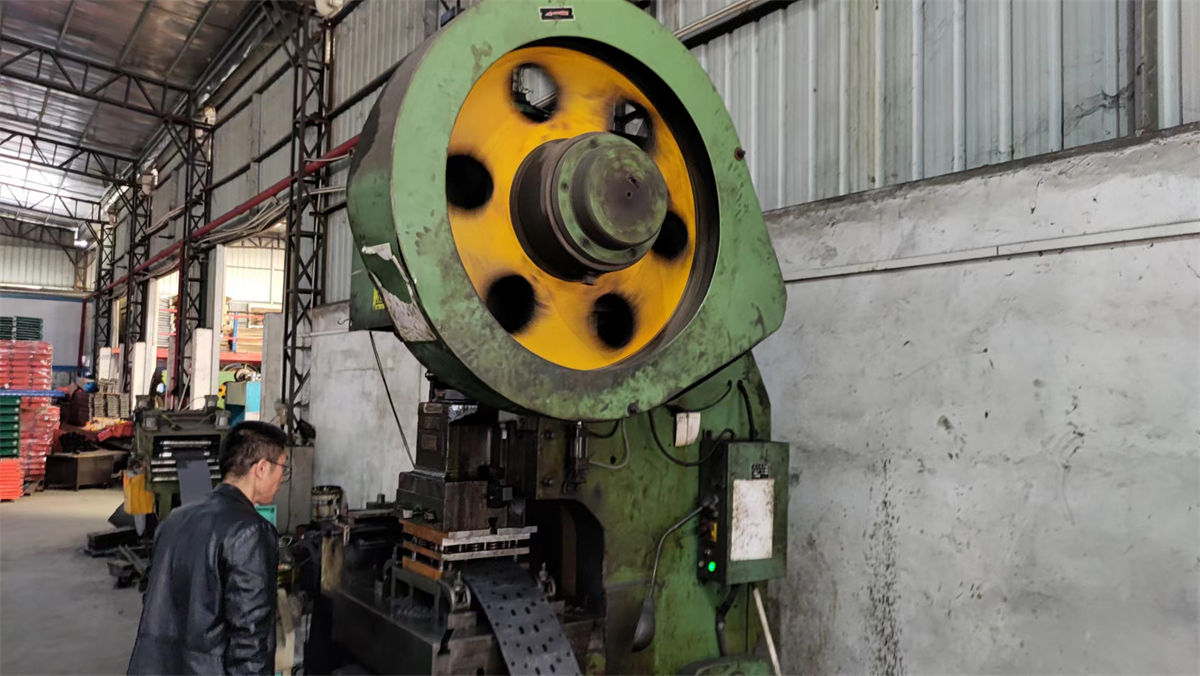
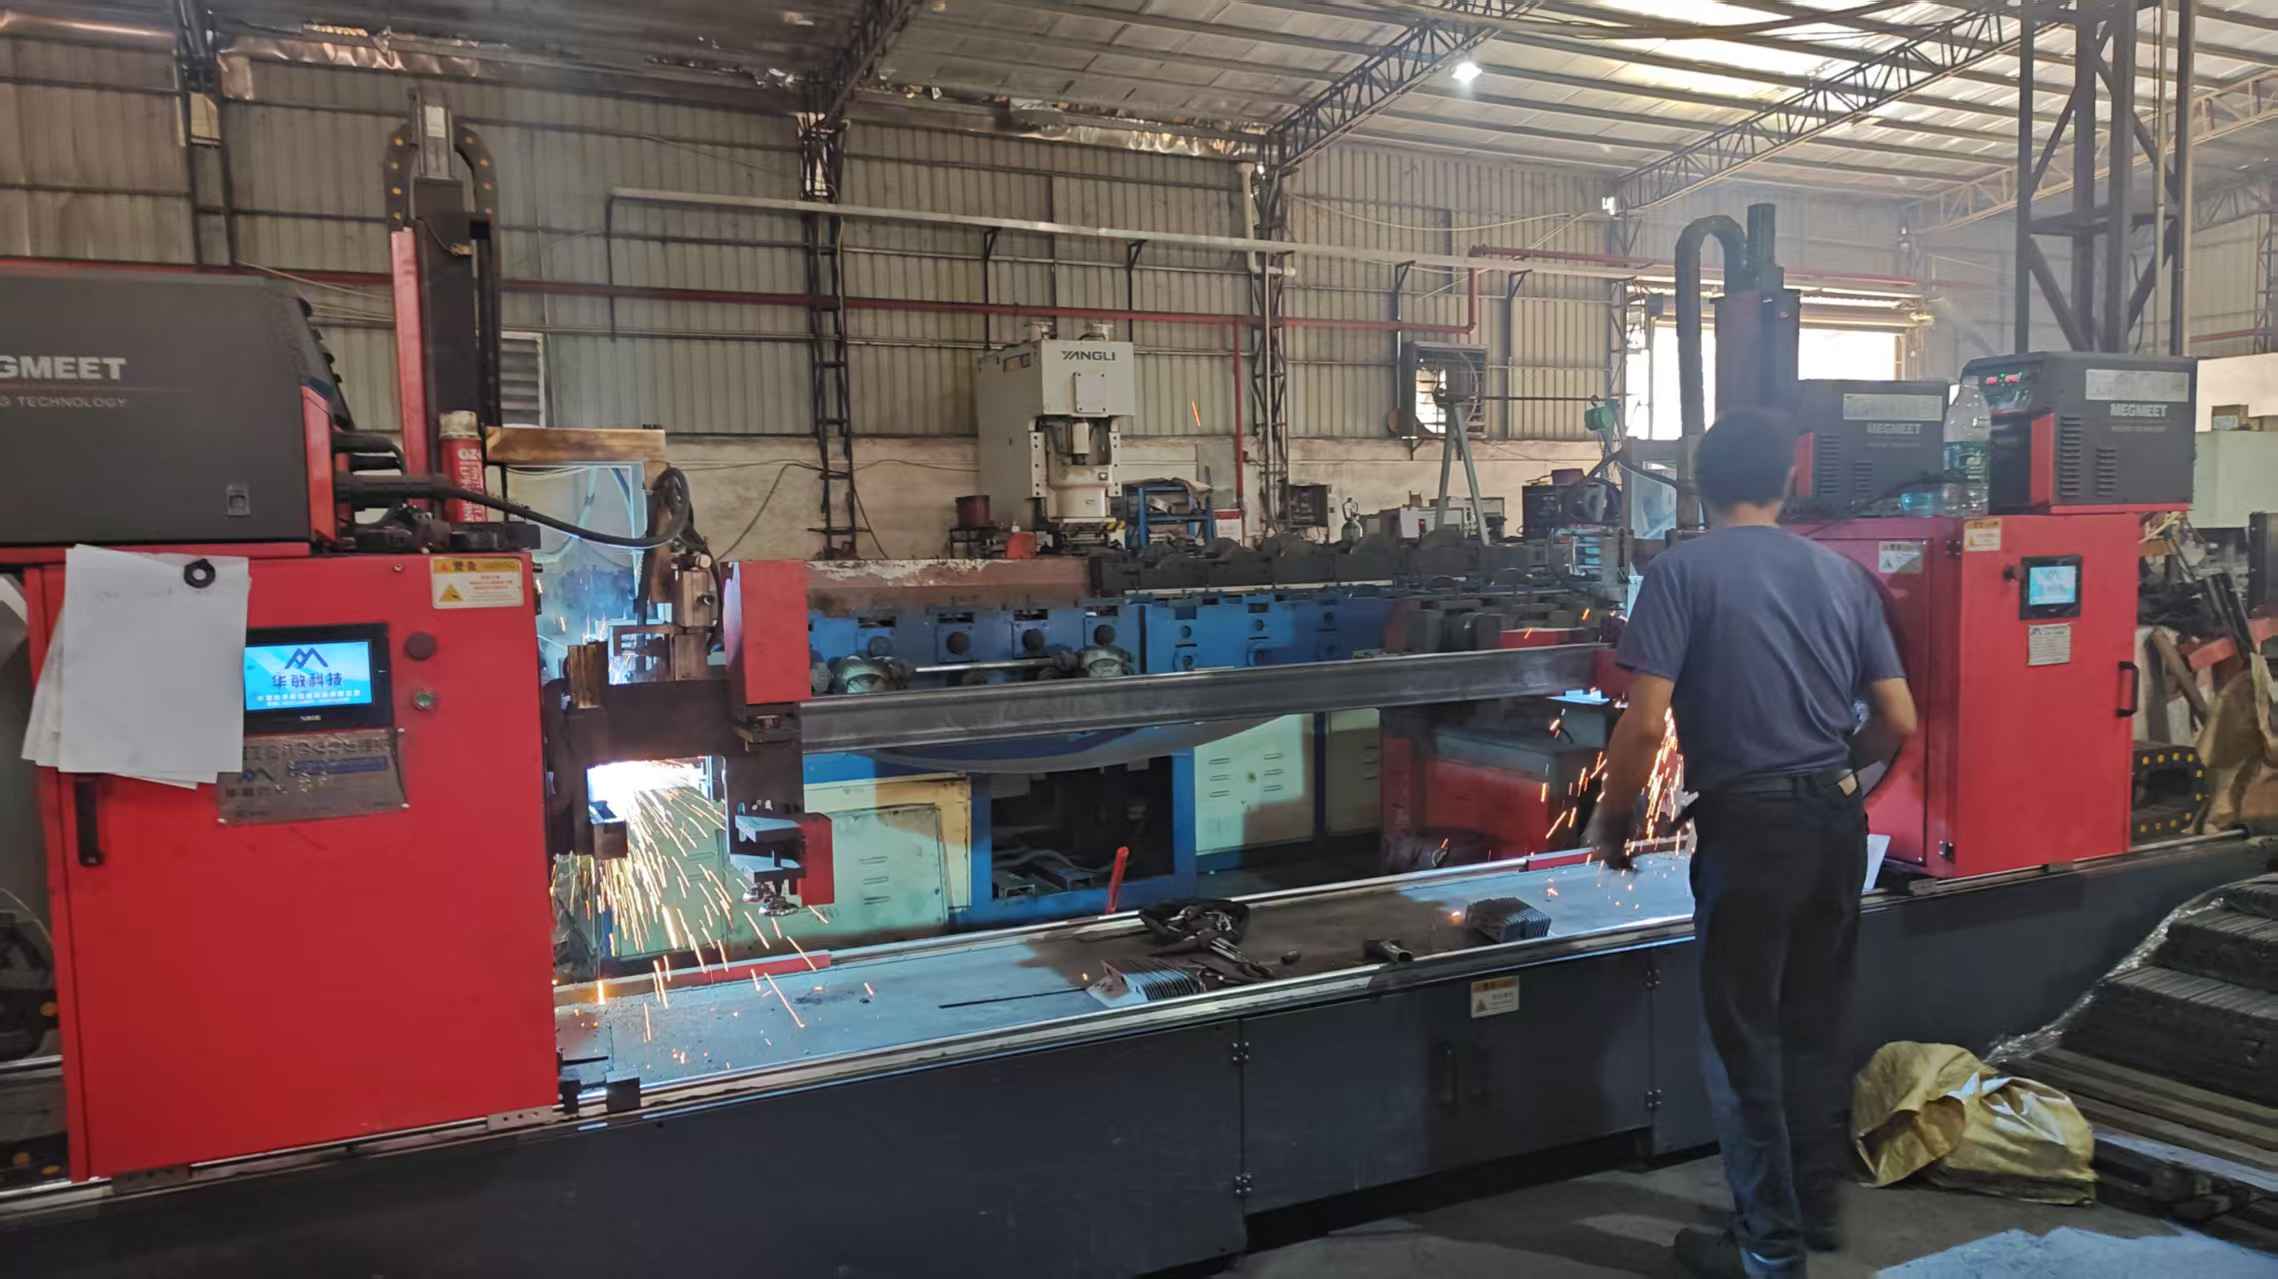
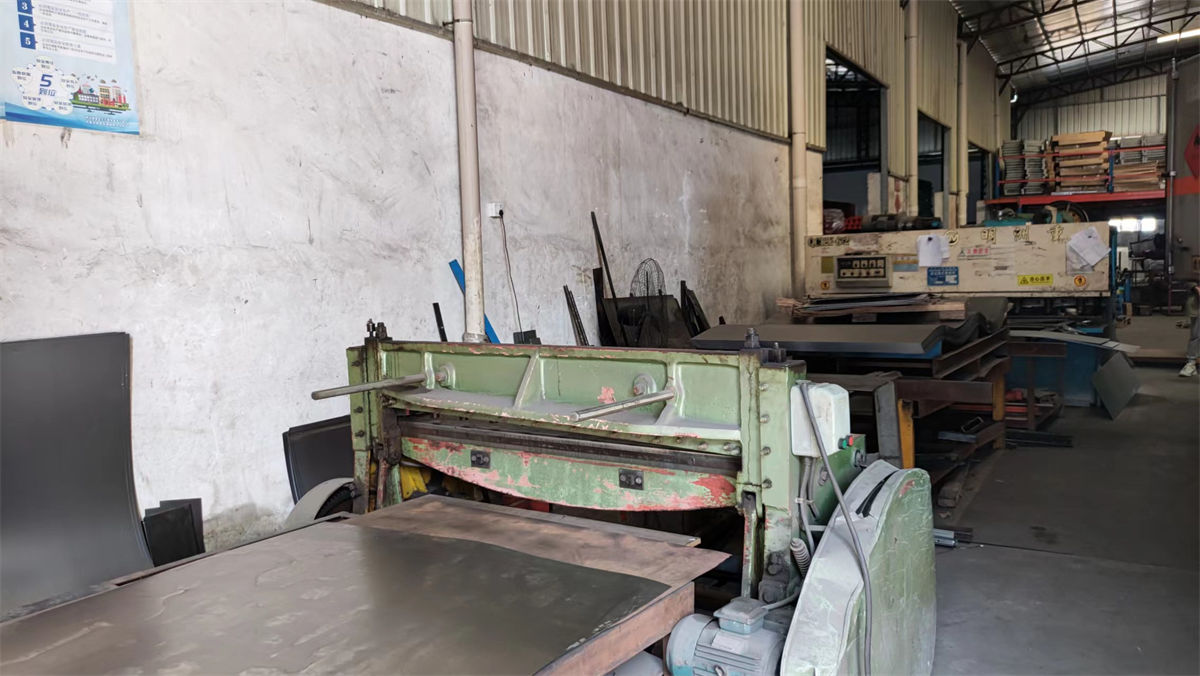
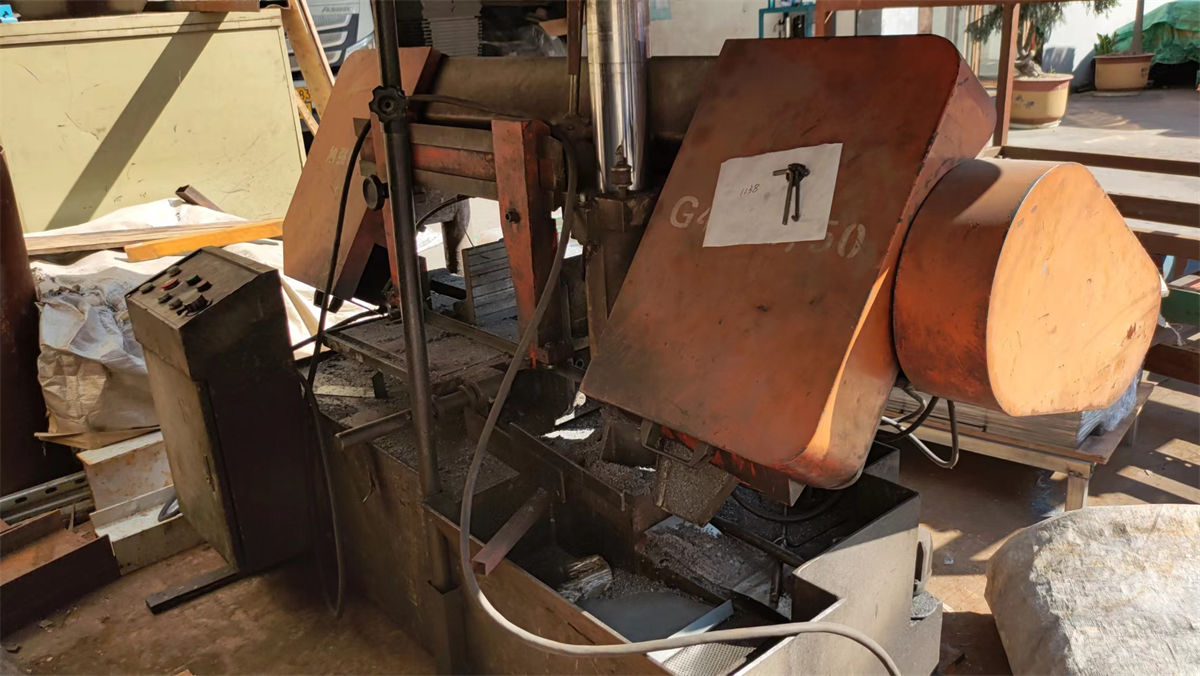
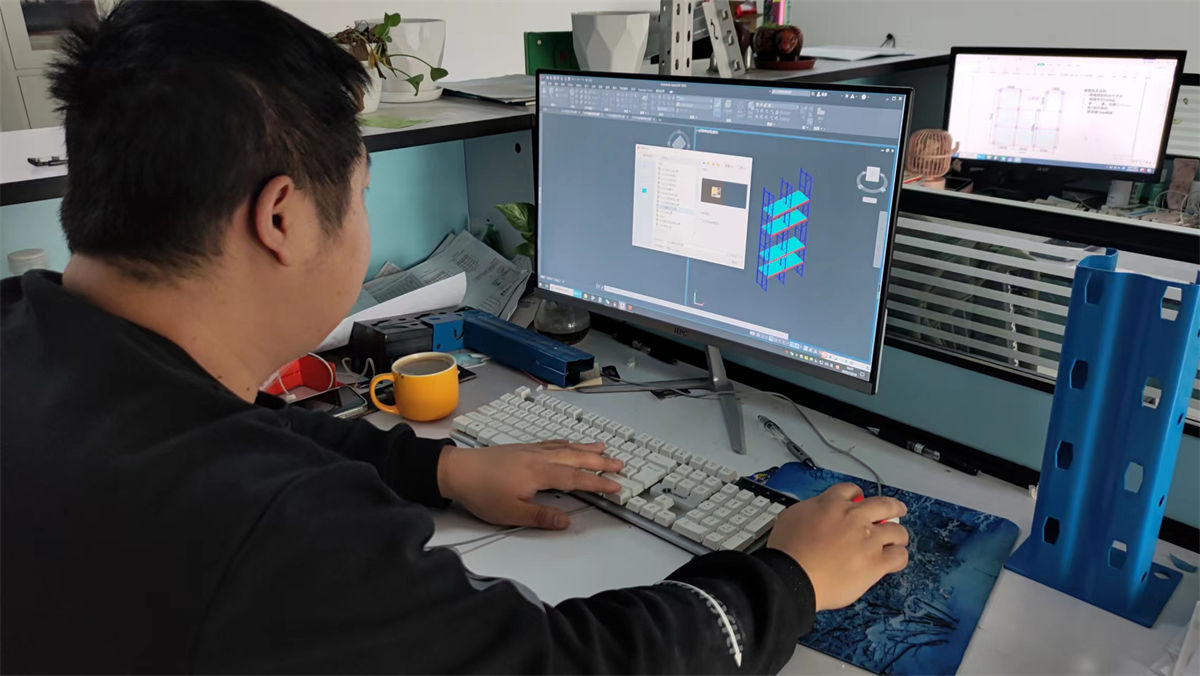
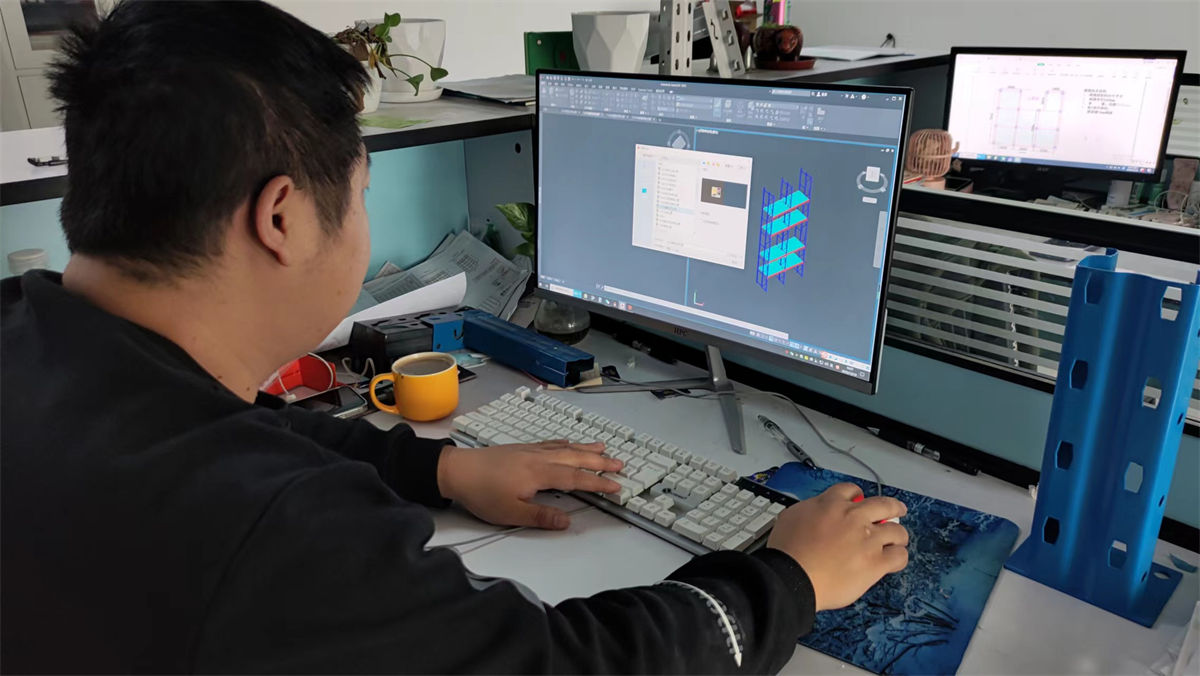
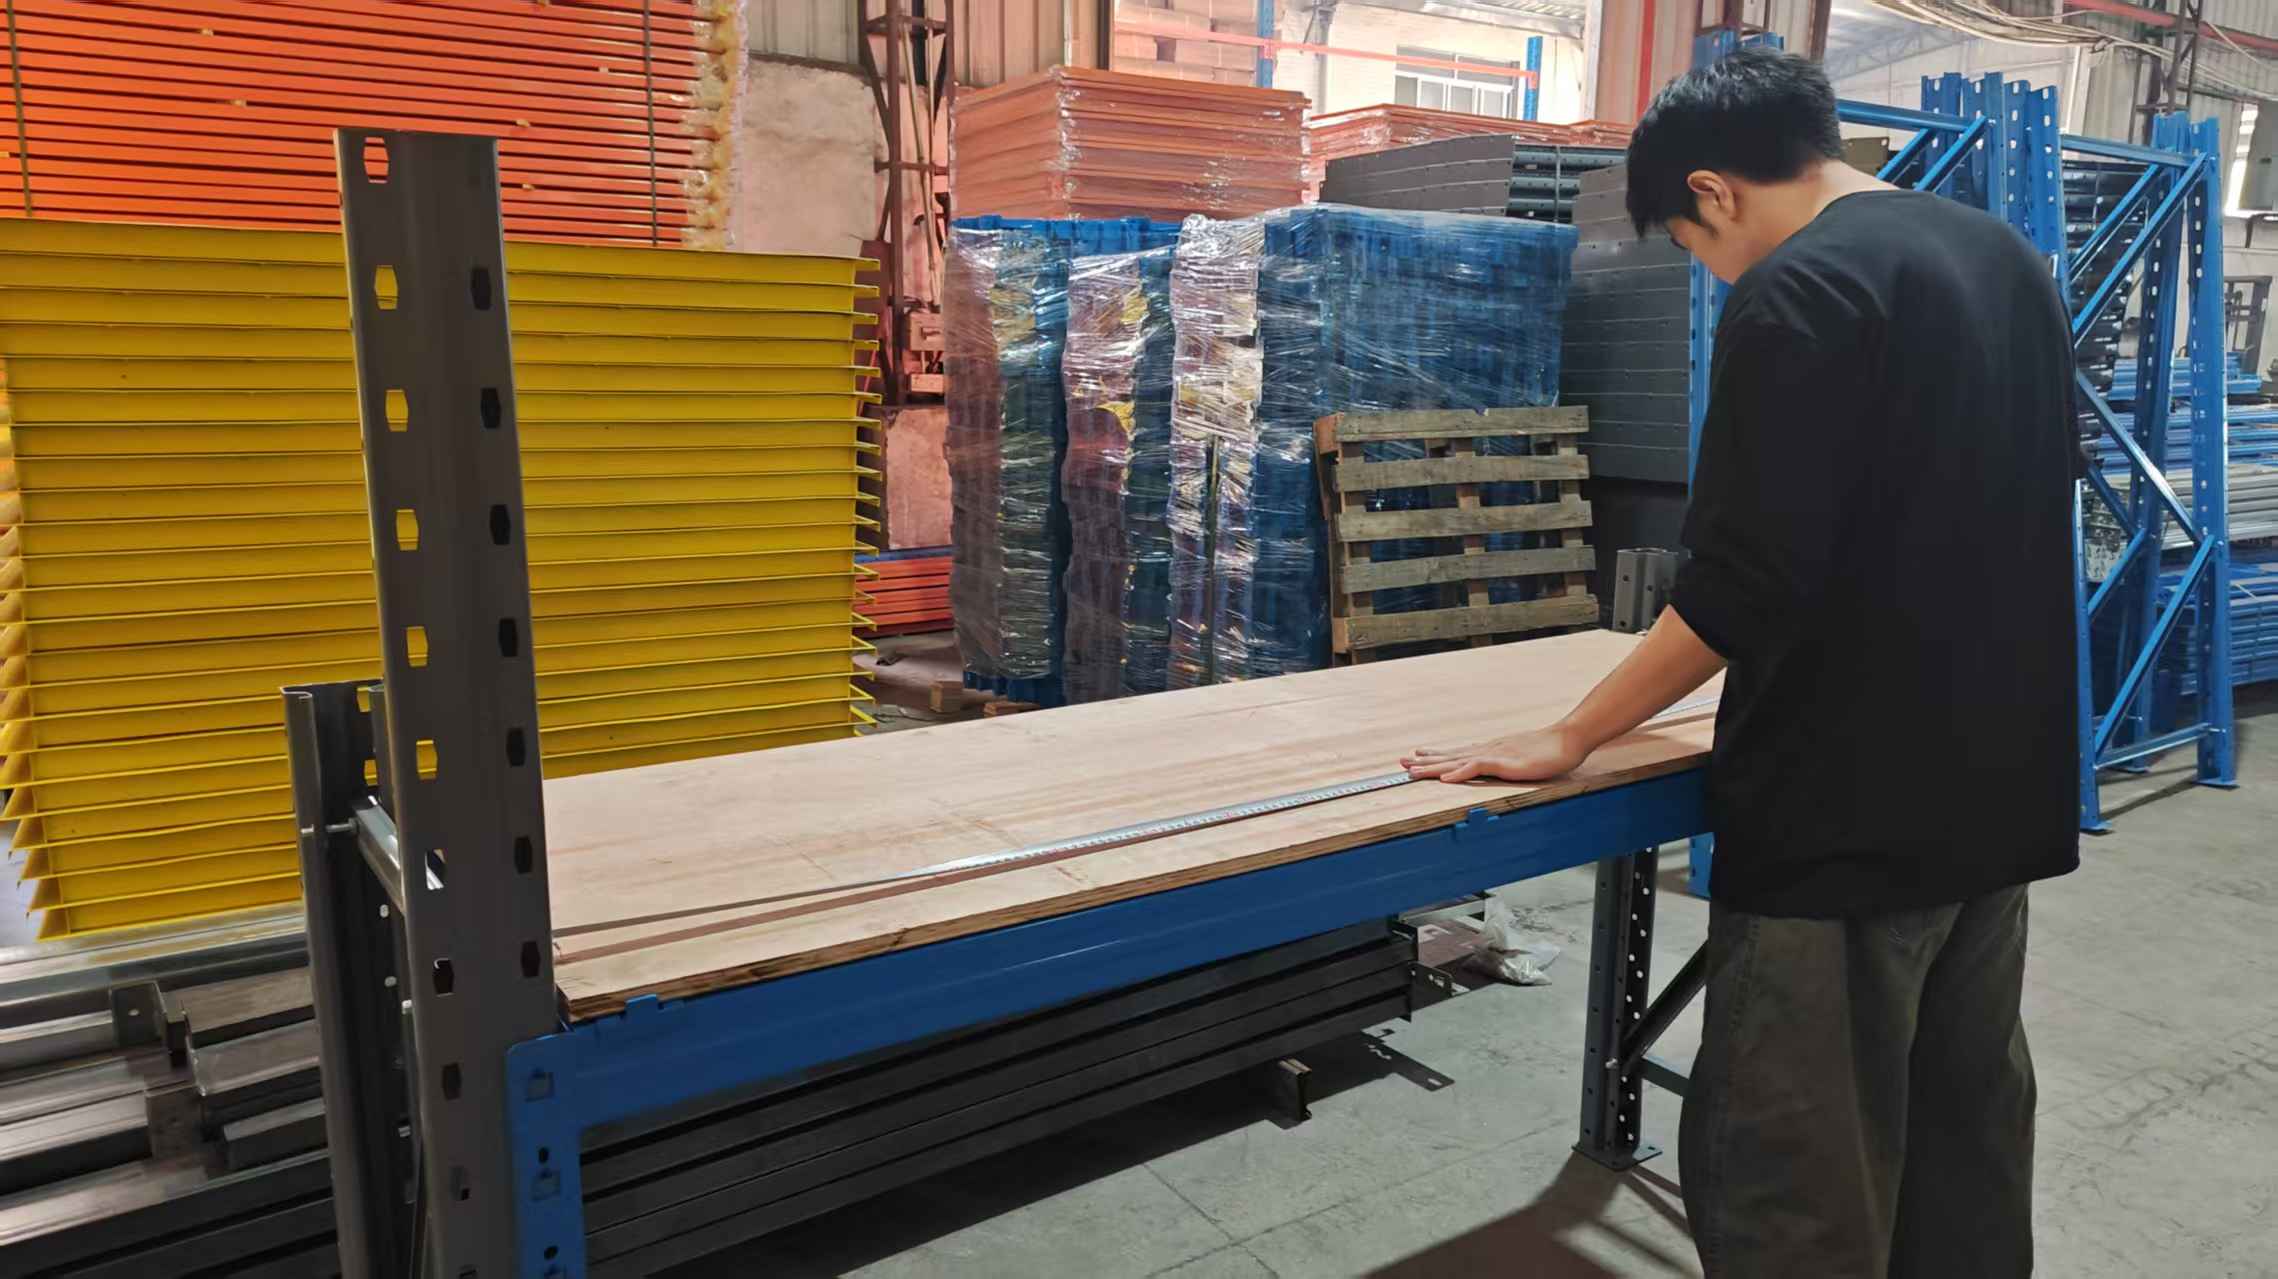
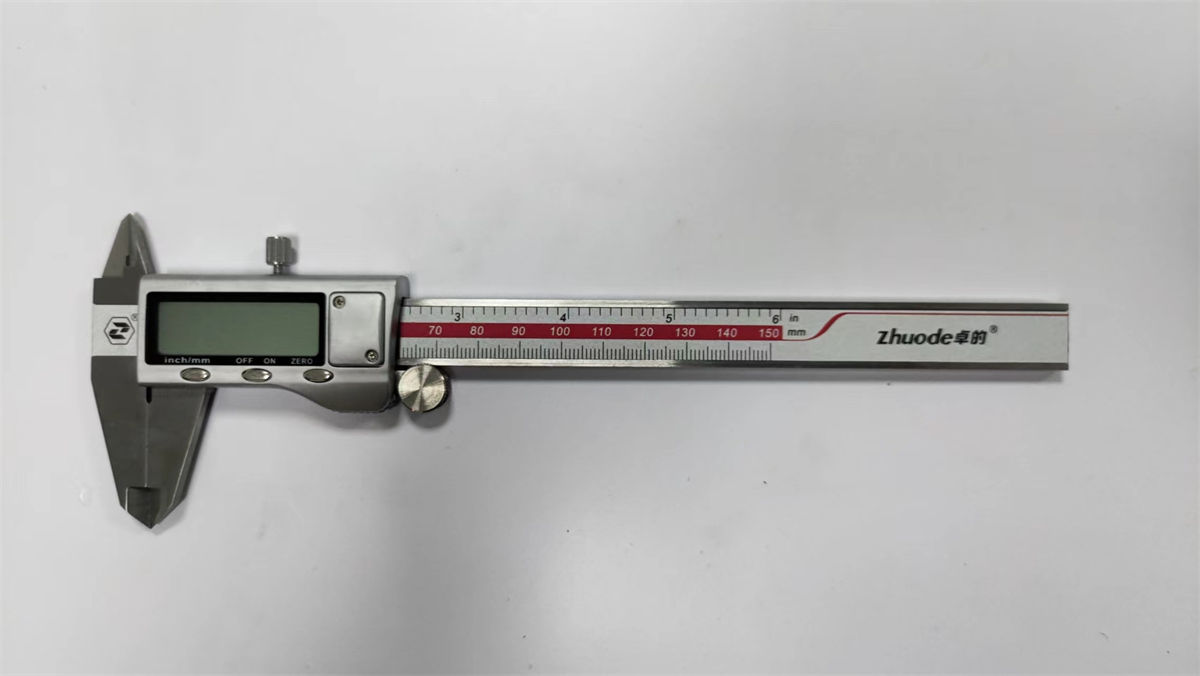
Discover our heavy-duty steel mezzanine floors, collapsible stack racks, and gravity flow racking systems.



Expert insights addressing common procurement, technical, and logistical inquiries for global warehouse storage systems.
 Xinmiao Racking